Bell & Gossett Pump Parts Diagram: Component Guide 2026
A Bell & Gossett pump parts diagram details the mechanical configuration of inline and base-mounted centrifugal pumps. It illustrates the spatial relationship between the volute casing, impeller, bearing assembly, shaft sleeve, spring coupler, and mechanical seal, allowing precise identification of wear components during system servicing and seal replacement.
📌 Key Takeaways
- Mechanical seal assemblies require precise shaft positioning and surface cleanliness to prevent fluid leaks.
- Volute gaskets and bearing assembly oil ring configurations vary according to pump series structure.
- Torque motor flange and volute casing bolts to 25–35 ft-lbs in a cross-pattern layout.
- The spring coupler and mechanical shaft seal represent the primary wear components during routine operation.
- Coupler and seal replacement can be performed DIY, but full motor rewinds require professional service.
Bell & Gossett centrifugal pumps serve as fundamental workhorses across commercial HVAC, industrial fluid transfer, and hydronic heating/cooling applications. Whether servicing a classic Series 100 inline circulator, a Series 60, or a heavy-duty e-1510 base-mounted end-suction pump, analyzing an accurate bell & gossett pump parts diagram is crucial for precise disassembly, component wear assessment, and exact replacement part sourcing. Technical schematics reveal the relationship between hydraulic wet-end assemblies and mechanical drive components. By understanding the structural alignment, mechanical seal positioning, bearing bracket tolerances, and fastener torque requirements illustrated in the blueprint, equipment mechanics and facility engineers can systematically execute rebuilds, eliminate fluid leaks, and extend equipment service life under demanding continuous-duty operating conditions.
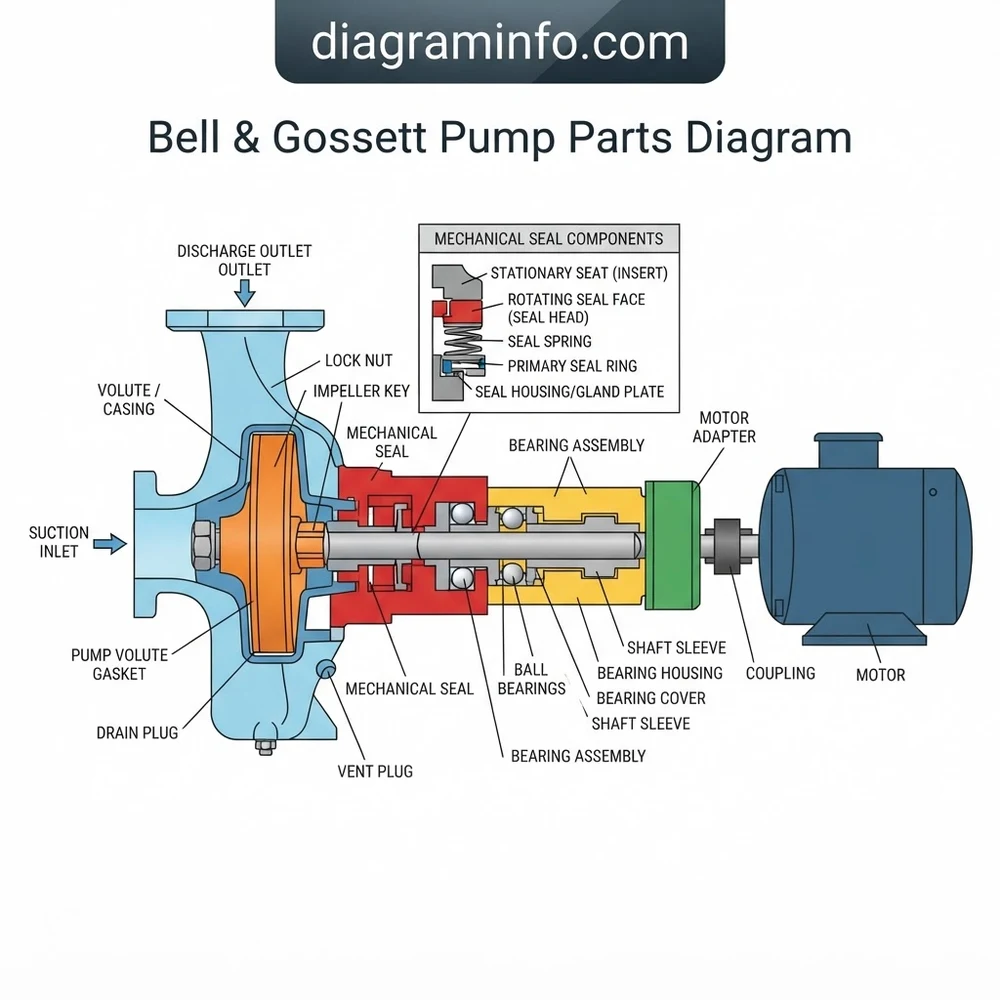
Bell & Gossett Pump Parts Diagram: Major Component Identification
A standard Bell & Gossett pump schematic illustrates an exploded view of the mechanical frame and fluid-handling structure. Understanding these components in detail ensures accurate identification during maintenance, allowing technicians to cross-reference OEM part numbers with specific physical dimensions and material grades before beginning a teardown.
1. Volute Casing (Pump Housing)
The volute casing acts as the primary fluid pressure containment vessel. It is engineered with a progressively expanding spiral contour that converts kinetic fluid velocity—imparted by the spinning impeller—into dynamic head pressure. Cast iron is standard for closed-loop hydronic heating systems, while lead-free bronze or 316 stainless steel casings are specified for open domestic potable water networks. The volute features integrated suction and discharge flanges, gauge tap ports, and bottom drain plugs.
2. Impeller and Impeller Retaining Hardware
The impeller is the primary rotating hydraulic component. Bell & Gossett utilizes enclosed backward-curved impellers, custom-trimmed to specific operating design points (head and flow requirements). The impeller mounts directly onto the shaft keyway or stepped shaft end and is held rigid by an impeller nut, washer, and lock washer combination. Impeller wear rings (or integral casing wear surfaces) maintain internal pressure isolation between the high-pressure discharge zone and the low-pressure suction eye.
3. Mechanical Seal Assembly
Positioned directly behind the impeller within the seal chamber, the mechanical seal prevents process fluid from escaping along the rotating shaft into the bearing housing. Standard industrial configurations utilize a Type 21 mechanical seal consisting of a stationary ceramic or silicon carbide seat, a rotating carbon ring, a Buna-N or EPDM elastomer bellows, and a stainless steel coil spring that maintains axial force across the sealing faces.
4. Shaft Sleeve and Bearing Assembly (Power Frame)
The shaft sleeve slips over the motor or pump shaft to shield it from fluid abrasion and chemical corrosion. In oil-lubricated models (such as the Series 100 or HV), the bearing assembly houses sleeve bearings, oil wicking material, thrust collars, and oil reservoir ports. Larger base-mounted series (such as the e-1510) utilize a heavy-duty power frame equipped with permanently sealed or regreasable deep-groove ball bearings engineered to handle high radial and dynamic hydraulic thrust loads.
5. Flexible Shaft Coupler and Motor Drive
The flexible coupler bridges the physical gap between the motor drive shaft and the pump bearing frame shaft. It compensates for minor parallel and angular misalignments while dampening torsional vibration. Configurations range from spring-loaded cast iron couplers on small circulators to flexible jaw inserts (EPR or polyurethane spiders) or Woods Sure-Flex grid couplings on higher-horsepower equipment.
Manufacturer specifications indicate maximum radial shaft runout must not exceed 0.002 inches TIR (Total Indicator Reading) at the seal seat face. Recommended volute cap screw torque for standard 3/8″-16 grade 5 bolts is 20–25 ft-lbs, while 1/2″-13 frame bolts require 45–50 ft-lbs applied in a cross-star pattern.
| Diagram Callout | Component Description | Standard Material Spec | Maintenance Consideration |
|---|---|---|---|
| P1 | Volute Casing | Cast Iron / Bronze / 316 SS | Inspect cutwater and internal surface for erosion or cavitation pitting. |
| P2 | Enclosed Impeller | Cast Bronze / Stainless Steel | Verify trim diameter against system curve; check wear ring clearances. |
| P3 | Mechanical Shaft Seal | Carbon/Ceramic/BUNA (Type 21) | Replace as a complete set. Never reuse lapped seal faces. |
| P4 | Shaft Sleeve | 304 Stainless Steel / Bronze | Check for micro-grooving; deep grooves cause premature seal leak. |
| P5 | Bearing Frame / Housing | Cast Iron Housing / Steel Shaft | Maintain oil level (20W non-detergent) or monitor grease interval. |
| P6 | Flexible Coupler Assembly | Steel / Cast Iron with Elastomeric Insert | Inspect for shear wear, dusting, or cracked spring arms during service. |
Analyzing Bell & Gossett Hydraulic Structure and System Layout

The structural configuration shown in a Bell & Gossett pump schematic highlights how mechanical energy transforms into fluid movement while isolating thermal and physical stress. Understanding the layout design differentiates inline circulators from frame-mounted end-suction models, dictating how forces travel through the pump system.
In close-coupled and inline series (such as the Series 100, HV, and 80/e-80), the overhung impeller layout relies on an integrated bearing assembly or extended motor shaft to absorb radial thrust loads. The hydraulic fluid enters axially through the suction flange at the center eye of the volute, turns 90 degrees outward through the rotating impeller passages, and discharges radially into the outer volute channel. Axial thrust is counterbalanced by balance holes drilled through the back shroud of the impeller, which equalize pressure between the suction eye and the seal chamber.
Base-mounted end-suction pumps (such as the Series 1510 and e-1510) utilize a true back-pullout configuration. The engineering blueprint reveals that the entire rotating assembly—including the bearing frame, seal chamber backplate, and impeller—can be removed from the volute housing without disturbing connected suction and discharge piping, or removing the motor if a spacer-type coupling is installed. For comprehensive teardown instructions on these power assemblies, review our detailed guide on bell & gossett bearing assembly rebuild methods.
According to OEM engineering specifications, hydraulic force inside the volute creates uneven radial thrust against the shaft at partial-flow operating conditions. Modern Bell & Gossett schematics account for this by incorporating optimized volute tongue (cutwater) clearances, reducing dynamic shaft deflection to under 0.001 inches at duty point performance.
How to Read the Bell & Gossett Pump Parts Diagram Step-by-Step

Interpreting a technical equipment blueprint requires a systematic methodology to ensure accurate disassembly, part sourcing, and rebuild procedures. Follow this step-by-step technical process when referencing a schematic during field service work.
Step 1: Locate and Cross-Reference Model Tag Identifiers
Before applying the schematic to physical hardware, check the metal nameplate located on the pump volute or bearing assembly. Record the complete Model Number, Part Number, and Revision Code (e.g., e-1510 2AD, Series 100 NFI). Match this data against the OEM parts catalog index. Minor variations in letter suffixes denote different seal materials, impeller ring clearances, or shaft sleeve dimensions.
Step 2: Trace the Rotating Assembly Alignment
Focus on the central centerline axis of the schematic layout. Trace the drive train starting from the motor shaft, moving through the flexible coupling, bearing shaft, shaft sleeve, mechanical seal, and ending at the impeller locknut. Note the spatial sequence of locking pins, snap rings, woodruff keys, and thrower rings. These secondary components maintain axial positioning and prevent components from shifting during high-torque startups.
Step 3: Analyze the Seal Chamber and Gasket Stack
Examine the mechanical seal expansion detail on the blueprint. Identify the stationary seal seat orientation relative to the backplate housing, and locate the primary body O-ring or volute gasket. Note whether the design uses a flush line piped from the volute discharge back to the seal chamber. Correct fluid circulation through this flush line is necessary to cool seal faces and clear entrained system debris.
Step 4: Verify Fastener Torque Patterns and Clearance Specs
Cross-reference callout numbers with the schematic fastener guide to confirm bolt lengths, thread pitches, and torque limits. Check the drawing for designated shim pack locations between the motor base and frame, which are critical for eliminating angular and parallel coupling alignment errors during final reassembly.
Never handle polished mechanical seal faces (carbon or ceramic) with bare hands. Skin oils contaminate the fine-lapped sealing surface, resulting in immediate micro-fissuring and fluid leakage upon system repressurization. Lubricate elastomeric bellows using approved non-petroleum lubricants (such as P-80 emulsion or soapy water) only.
Troubleshooting Mechanical Failures Using System Blueprints
When hydronic systems exhibit physical leakage, low flow performance, or elevated noise levels, referring to a bell & gossett pump parts diagram enables targeted diagnostic routines. Below are common mechanical failure modes mapped directly to schematic component locations.
1. Persistent Fluid Leakage from the Seal Chamber Backplate
If fluid drips continuously from the bottom drain slot of the bearing frame or backplate bracket, the mechanical seal faces have degraded, or the shaft sleeve has grooved.
Diagnostic Method: Isolate the pump, drain the volute, and remove the back-pullout assembly. Inspect part reference P3 (Seal Assembly) and P4 (Shaft Sleeve) on your schematic. Check the shaft sleeve for scored channels exceeding 0.005 inches deep. If scored, replacing the mechanical seal without replacing the sleeve will cause the new elastomeric bellows to fail immediately. Refer to our mechanical seal maintenance guide for step-by-step seal face lapping and insertion procedures.
2. Excessive High-Frequency Vibration and Bearing Overheating
Vibration accompanied by high temperature at the bearing bracket (exceeding 180°F/82°C) typically indicates angular coupler misalignment, bent shafts, or degraded bearing races.
Diagnostic Method: Reference coupler positioning on the layout diagram. Remove the coupler guard and measure parallel offset using a dial indicator mounted on the motor shaft hub. If offset exceeds 0.004 inches, unbolt the motor and re-shim the base. For oil-lubricated bearing assemblies (e.g., Series HV), verify that the internal oil wicks are saturated with non-detergent SAE 20W oil and are physically contacting the rotating shaft journal.
3. Hydraulic Performance Loss (Reduced Flow and Head Pressure)
When the pump operates at rated RPM but fails to generate design differential pressure, internal recirculation is occurring within the volute.
Diagnostic Method: Consult the impeller and wear ring details on the blueprint layout. Measure the radial clearance between the impeller eye hub and the casing wear ring using feeler gauges. Standard factory clearance ranges between 0.010 and 0.015 inches. If wear ring erosion expands this clearance beyond 0.030 inches, high-pressure discharge water short-circuits back into the suction eye, severely degrading pump performance. If pressure instability persists along with gravel-like rumbling noises, consult our technical resource on hydronic pump cavitation diagnosis to distinguish between physical component wear and suction-side net positive suction head (NPSH) starvation.
Bell & Gossett Pump Parts Diagram Frequently Asked Questions
How do I determine the correct mechanical seal material for my Bell & Gossett pump schematic?
Mechanical seal selection depends on system fluid composition, glycol concentration, and operating temperatures. Standard BUNA-N/Carbon/Ceramic seals (Code B) are rated up to 225°F (107°C) for clean water systems. Systems containing over 30% propylene glycol or operating at temperatures up to 250°F (121°C) require an EPDM/Carbon/Silicon Carbide seal arrangement (Code E or S). Always match the seal suffix listed on the pump identification tag to the parts manual legend.
What is the correct oil capacity and fluid type for oil-lubricated bearing assemblies?
Small-to-medium oil-lubricated Bell & Gossett bearing frames (Series 100, HV, PR, 2″) utilize high-grade non-detergent SAE 20W turbine/bearing oil. Fill the bearing reservoir through the top oil cup until the oil level reaches the center of the side oil-level gauge plug or sight glass. Overfilling causes oil churn, leading to excessive thermal expansion, seal degradation, and premature bearing failure.
Why does my flexible coupler shear or wear out rapidly after replacement?
Coupler shear is almost universally caused by excessive shaft misalignment between the motor drive shaft and the pump bearing shaft, or by severe system thermal expansion placing stress on pump piping flanges. Using a straightedge or dial indicator, align the pump and motor shaft hubs within 0.002 inches total indicator reading for both axial parallel offset and angular face alignment before installing the elastomeric coupler body.
Can I install a larger impeller diameter than what is shown on my original pump tag layout?
An impeller can only be expanded up to the maximum internal volute cutwater clearance indicated on the specific pump frame model schematic. Furthermore, increasing impeller diameter increases motor brake horsepower (BHP) requirements exponentially (following proportional affinity laws). Increasing impeller diameter without verifying motor nameplate full-load amp (FLA) ratings and service factors will cause thermal overload tripping on the electrical supply circuit.
What is the functional difference between an exploded view layout and a hydraulic schematic?
An exploded view blueprint depicts physical mechanical relationships, individual component part numbers, fastener sequences, and assembly spatial orientation required for physical teardown and repair. A hydraulic schematic represents the overall system fluid loop using standardized symbols to indicate piping layout, isolation valves, check valves, triple-duty valves, strainers, and pressure tap points without detailing internal mechanical construction.