Cat Pump 66DX40G1 Parts Diagram: 2026 Repair Guide
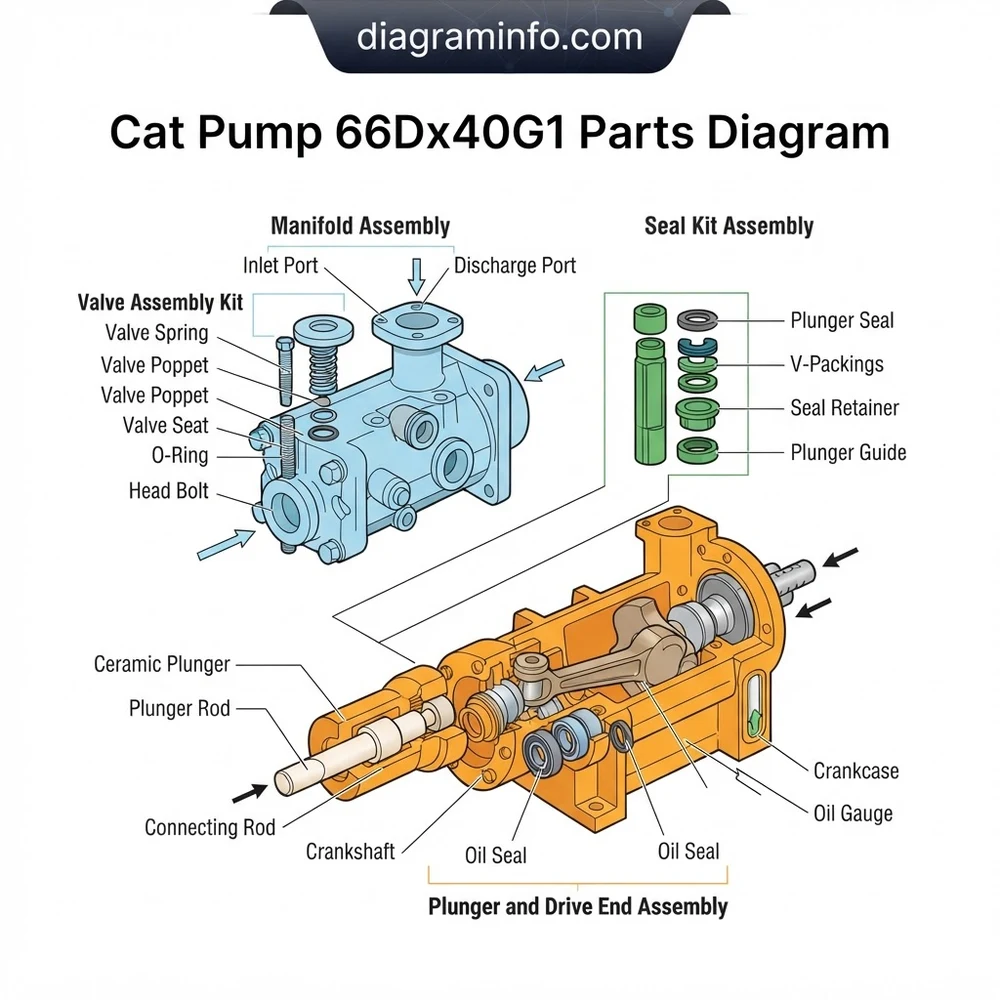
The Cat Pump 66DX40G1 parts diagram details the layout for this 4.0 GPM, 4000 PSI axial plunger pump. It features a brass manifold section housing inlet/discharge valve assemblies (Kit 76302) and high-pressure ceramic plunger seals (Kit 76307), attached to an aluminum crankcase housing the crankshaft and swash plate driver assembly.
📌 Key Takeaways
- Cat Pump 66DX40G1 delivers 4.0 GPM at 4000 PSI with a 1-inch hollow shaft rated for 3400 RPM gas engines.
- Valve kit 76302 and seal kit 76307 represent the most frequent service replacement components shown on the layout.
- Manifold hex bolt torque must be maintained at 125 in-lbs (14.1 Nm) during reassembly to prevent high-pressure fluid leakage.
- Worn low-pressure seals or cracked ceramic plungers are the leading causes of pressure drop and crankcase oil contamination.
- DIY seal and valve kit replacement is straightforward, but internal swashplate bearing failure requires professional overhaul.
The Cat Pump 66DX40G1 is a direct-drive, industrial-grade triplex plunger pump designed for high-pressure washing systems powered by 1-inch hollow shaft gasoline engines. Operating at a maximum flow rate of 4.0 GPM (15.1 L/min) and pressures up to 4000 PSI (275 bar) at 3400 RPM, this pump relies on strict dimensional tolerances and durable internal metallurgy. Understanding the precise cat pump 66dx40g1 parts diagram is critical for equipment technicians and mechanics tasked with executing routine seal replacements, valve overhauls, or full crankcase repairs. This technical guide provides a deep-dive analysis of the pump’s structural layout, component cross-references, schematic interpretation techniques, and systematic troubleshooting procedures using original manufacturer specifications.


Cat Pump 66DX40G1 Parts Diagram and Structural Component Layout


According to OEM engineering documentation, the Cat Pump 66DX40G1 architecture is segregated into two primary structural sections: the wet end fluid manifold assembly and the dry end crankcase drive system. The fluid head utilizes a high-density forged brass manifold engineered to absorb recurring hydraulic shock loads up to 4000 PSI. Integrated into this manifold structure are six individual valve assemblies—three suction valves situated in the lower fluid chambers and three discharge valves housed directly above the plunger chambers. The pump features an integrated pressure-regulating unloader valve mounted directly to the manifold body, which diverts fluid flow during trigger-gun bypass cycles to eliminate thermal over-pressurization.
The mechanical drive end features a high-strength aluminum alloy crankcase with a precision-machined oil reservoir holding exactly 18 ounces of non-detergent ISO 68 hydraulic oil. A hardened chrome-moly steel crankshaft transfers mechanical torque through three die-cast aluminum connecting rods to crosshead pin assemblies. High-purity, solid ceramic plungers attach to stainless steel plunger rods, traversing dual-stage oil and high-pressure fluid seals. The dual-sealing configuration employs a low-pressure seal to retain crankcase lubrication and a high-pressure seal with a elastomeric V-packing structure designed to withstand severe fluid velocities.
Cat Pump Model 66DX40G1 OEM Specs: Max Flow: 4.0 GPM (15.1 L/min) | Max Pressure: 4000 PSI (275 bar) | Max Speed: 3400 RPM | Engine Mounting Shaft: 1.0 Inch Hollow Shaft (Gasoline Engine Flange SAE J609a) | Crankcase Oil Capacity: 18.0 oz (0.53 L) ISO 68 Non-Detergent | Max Fluid Temperature: 140°F (60°C) | Inlet Port: 1/2″ NPT(F) | Discharge Port: 3/8″ NPT(F).
Manifold Head and Valve Assembly Configuration
The hydraulic manifold structure houses six stainless steel valve assemblies arranged in vertical pairs across the three pumping channels. Each valve unit comprises a stainless steel spring retainer, a tempered stainless steel spring, a precision-ground valve seat, a valve poppet, and an elastomeric O-ring seat seal. Manufacturer specifications indicate that valve seat wear directly impacts output GPM; therefore, these units are grouped together under standard service kits. Adjacent to the valve seats are the high-pressure packing assemblies, which utilize a brass intermediate seal retainer, a high-pressure V-packing seal, and a low-pressure fluid seal ring. Proper indexing of these components according to the structural schematic prevents internal cavitation and high-pressure blow-by.
Crankcase Drive End and Plunger Rod Structure


The internal mechanical drive layout consists of a forged crankshaft seated within heavy-duty ball bearings pressed into the aluminum crankcase cover. Three precision-ground ceramic plungers slide through oil retainers into the fluid manifold. Solid ceramic plungers are selected for their thermal resistance and wear characteristics, preventing micro-abrasions that could otherwise shred high-pressure seals. The mechanical interface utilizes crosshead guides pinned to connecting rods, which press against oil seals mounted in the crankcase body wall. Maintaining structural integrity within this region requires monitoring oil level via the rear-mounted sight glass and ensuring that the oil cap breather remain unobstructed during operation.
Built-in Unloader Valve and Pressure Regulator System
The 66DX40G1 features a factory-fitted, built-in unloader valve assembly integrated into the fluid manifold casting. The unloader system incorporates a spring-loaded bypass piston, a check valve, and an adjustable pressure knob control. When the discharge gun trigger is released, build-up of backpressure shifts the unloader piston, opening an internal bypass circuit that recirculates water back to the suction side of the pump manifold. This prevents mechanical overloading of the gas engine driver while maintaining stable internal hydraulic pressure within set limits.


| Callout Ref | Component Description | OEM Part Number | Torque / Fit Spec | Material Construction |
|---|---|---|---|---|
| Ref 127 | Manifold Head Bolt (M8 x 65) | PN 125824 | 17.3 ft-lbs (23.5 Nm) | Plated High-Tensile Steel |
| Ref 163 | Complete Valve Kit (6 per pump) | PN 34023 / 76023 | Hand Seat Seal Installation | 304 Stainless Steel / NBR |
| Ref 164 | High-Pressure Seal Kit | PN 34021 / 76021 | Pre-lubricated Press Fit | NBR / High-Density PTFE |
| Ref 48 | Solid Ceramic Plunger (14mm) | PN 48394 | 7.0 ft-lbs (9.5 Nm) Nut | Alumina Ceramic |
| Ref 163 Plugs | Valve Plug Caps (M20) | PN 48385 | 37.0 ft-lbs (50.0 Nm) | Forged Brass |
| Ref 10 | Crankcase Cover Bolt (M6) | PN 126543 | 8.2 ft-lbs (11.1 Nm) | Zinc-Plated Steel |
How to Read the Cat Pump 66DX40G1 Parts Diagram for Overhauls


Interpreting a cat pump 66dx40g1 parts diagram requires a systematic approach to reading numerical callouts, exploded-view spatial relationships, and sub-assembly groupings. The diagram utilizes standard numerical referencing wherein key numerical clusters correspond directly to specific system regions. For instance, single and double-digit callout numbers (1-90) designate drive-end crankcase, rod, and crankshaft mechanics. Numbers in the 100 series (100-190) denote wet-end fluid head components, including seals, plungers, and manifold fasteners. Numbers above 400 reference the integral unloader valve configuration and external bypass plumbing.
When preparing for an overhaul, technical technicians must cross-reference part callout numbers with the pump service kit key. Cat Pump supplies service kits rather than individual O-rings for critical rebuild steps to guarantee correct material hardness (Durometer rating) and thermal tolerances. Referencing the schematic layout ensures components are oriented correctly—specifically paying attention to the directional lip seal orientation on low-pressure seals and the elastomeric V-packing curvature on high-pressure seals, both of which must face toward the high-pressure manifold chamber.
When servicing the wet end, always cross-reference pressure washer pump repair guides to ensure the engine keyway aligns with the hollow shaft drive key. Failure to apply anti-seize lubricant onto the engine shaft prior to mounting can result in severe galling and shaft lockup.
Interpreting Callouts and Exploded View Fasteners


On the structural blueprint, solid lines connecting components indicate direct mechanical mating or press-fit positioning, whereas dashed projection lines demonstrate the axial assembly order along the plunger stroke centerline. Fasteners are labeled with specific thread pitch and diameter values (e.g., M8 x 65 for manifold bolts). Following the exploded view from left to right establishes the disassembly order: removing external manifold caps first, extracting internal valve components next, and detaching the forged manifold block from the crankcase frame last. This logical structure prevents cross-threading or applying uneven mechanical tension to ceramic plungers during teardown.


Systematic Disassembly Sequence Using System Blueprints
To safely execute a complete wet end teardown using the technical diagram as a guide, follow these precise mechanical procedures:
- Step 1: Relieve Pressure and Drain Oil. Disconnect fluid supply lines. Unbolt the bottom crankcase drain plug (Ref 32) using an 8mm allen wrench to drain all 18 ounces of pump oil into an approved container.
- Step 2: Remove Valve Plug Caps. Using a 22mm socket, unscrew the six valve plugs (Ref 163) exposed on the top and front face of the forged manifold block.
- Step 3: Extract Valve Assemblies. Using needle-nose pliers, extract the six valve assemblies (Ref 163 kit). Inspect each valve seat and poppet for pitting, wire-drawing, or spring fracture.
- Step 4: Detach Manifold Block. Remove the eight outer M8 socket-head cap screws (Ref 127) using a 6mm Allen socket. Slide the manifold head straight forward off the ceramic plungers to prevent lateral shear stress on the ceramic sleeves.
- Step 5: Pull Seal Retainers and Packing Seals. Slide the high-pressure seal retainers, V-packings, and low-pressure seals out of the manifold seal cavities. Inspect ceramic plungers (Ref 48) for score marks, cracking, or thermal fractures.
Reassembly Torque Specifications and Seal Alignment


Reassembly must strictly adhere to the manufacturer’s torque sequences detailed in the schematic documentation. When installing replacement high-pressure seals (Kit PN 34021), apply a thin coat of silicone-based grease to the seal lips. Never use petroleum-based grease on NBR or EPDM elastomers, as it causes swelling and premature seal failure. Slide the seal assemblies onto the plunger guide using an insertion tool to keep the sealing lips flat.
Reinstall the brass manifold over the ceramic plungers horizontally. Tighten the eight M8 manifold cap screws in a criss-cross star pattern to ensure even clamping pressure across the sealing surfaces. Torque each bolt in two stages: first to 10 ft-lbs (13.5 Nm), and final torque to 17.3 ft-lbs (23.5 Nm). Reinstall valve assemblies with new O-rings, applying 37.0 ft-lbs (50.0 Nm) of torque to the valve plug caps.
Diagnosing Hydraulic Failure Modes Using the System Schematic


System failures on the Cat Pump 66DX40G1 generally manifest as pressure drop, fluid leakage, or mechanical knocking within the crankcase drive end. Utilizing the component schematic allows technicians to trace symptoms back to specific failure modes within the pump layout. Mechanical diagnosis requires systematically isolating whether an issue originates in the low-pressure inlet hydraulics, high-pressure discharge circuits, or drive end mechanical linkages.
Operating the pump above 4000 PSI or running the pump dry without water flow for more than 90 seconds will cause rapid thermal expansion, destroying ceramic plungers and high-pressure seals. Always verify full water supply flow before starting the engine.
Pressure Loss and Internal Bypass Faults
A sudden drop in operating pressure despite full engine RPM usually points to compromised valve components or unloader seat erosion. Referring to the manifold schematic, inspect the internal check valve poppet and seat within the integrated unloader valve assembly (Ref 400 series). A trapped piece of debris under a discharge valve seat (Ref 163) prevents the valve poppet from sealing, causing fluid to bypass internally between adjacent chambers. If the engine labors while pressure remains low, the unloader bypass valve stem is likely stuck in the full bypass position due to scale deposits or worn O-rings.
Milky Crankcase Oil and Water Seal Degradation
The presence of milky, emulsified oil inside the crankcase sight glass indicates water intrusion past the low-pressure fluid seals and oil retainers. Tracing the plunger shaft axis on the diagram shows two barrier seals: the high-pressure packing seal, which holds fluid in the manifold, and the low-pressure crankcase oil seal (Ref 56), which keeps water out of the crankcase reservoir. When high-pressure seals wear out, water under pressure sprays back along the ceramic plunger shaft. If the oil slinger ring or low-pressure seal is degraded, water penetrates the crankcase housing, diluting the lubricant. Continuous operation with contaminated oil damages the internal connecting rods and crankshaft bearings within hours.


Cavitation and Fluid Delivery Cavity Restricting
Hydraulic knocking or severe vibration in the discharge hose is a classic indicator of pump cavitation. Cavitation occurs when the pump is starved of water at the inlet port (1/2″ NPT), creating vacuum voids that collapse violently against the ceramic plungers and valve seats. Reviewing the inlet flow layout indicates that restricted supply lines, clogged inlet filters, or undersized inlet hoses (less than 5/8″ ID supply hose) cause uneven chamber filling. Consult triplex plunger pump maintenance protocols to verify supply GPM and inlet vacuum levels before replacing internal mechanical components.
Cat Pump 66DX40G1 Maintenance and Assembly Specifications FAQ
What type of oil is required for the Cat Pump 66DX40G1 crankcase, and how often should it be changed?
The Cat Pump 66DX40G1 requires exactly 18.0 oz. (0.53 L) of specially formulated ISO 68 non-detergent hydraulic fluid (Cat Pump Custom Blend Oil PN 6107). Standard automotive motor oil must never be used because its detergent additives entrain air and absorb moisture, accelerating oxidation and bearing wear. Perform the initial break-in oil change after the first 50 hours of operation. Subsequent oil service intervals must occur every 300 operating hours or every 3 months, whichever comes first.
How do I adjust the integrated unloader valve to achieve full 4000 PSI pressure?
Pressure adjustment is performed with the gas engine running at full governed speed (3400 RPM) with the discharge spray gun attached and open. Thread the red pressure adjusting knob clockwise to increase system working pressure or counter-clockwise to lower it. Monitor an accurate, liquid-filled pressure gauge mounted on the discharge port. Turn the knob until the gauge reaches the rated 4000 PSI mark while spraying. Ensure that when the spray gun trigger is released, the spike pressure does not exceed 4400 PSI before the valve transitions to full bypass. Adjusting industrial unloader valve tuning procedures ensures the jam nut is locked in place after final setting.
What are the exact part numbers for the seal kit and valve kit on the 66DX40G1?
The standard complete valve overhaul kit for all six valves is OEM Part Number 34023 (or 76023 for high-temperature options). The complete high-pressure water seal overhaul kit for all three plunger channels is OEM Part Number 34021 (or 76021). If replacing individual ceramic plungers, order Part Number 48394 (14mm diameter solid ceramic plunger sleeve).
How do I replace cracked ceramic plungers using the parts schematic?
To replace a ceramic plunger, unbolt and remove the fluid manifold head following the disassembly sequence. Locate the plunger retainer nut at the exposed end of each plunger assembly. Unscrew the plunger nut (Ref 47) counter-clockwise using a 10mm socket. Remove the copper washer, solid ceramic sleeve (Ref 48), and underlying O-ring. Inspect the exposed plunger rod for scoring. Clean the mounting stud thoroughly, install a new shaft O-ring, slide the new ceramic plunger sleeve into position, replace the copper washer, and apply Threadlocker to the plunger nut before torquing to exactly 7.0 ft-lbs (9.5 Nm).
What gas engine engine shafts are compatible with the 66DX40G1 mounting flange?
The 66DX40G1 features a standard SAE J609a direct-drive mounting flange designed specifically for horizontal gas engines rated between 9 HP and 15 HP (such as the Honda GX270 or Honda GX390). The engine crankshaft must have a precise 1.0-inch (25.4mm) straight shaft diameter with a standard 1/4-inch square keyway. The pump hollow shaft slides directly over the engine shaft and is secured using four 3/8″-16 UNC mounting bolts torqued to 15 ft-lbs (20.3 Nm).
Step-by-Step Guide to Understanding the Cat Pump 66Dx40G1 Parts Diagram
Identify – Locate the cat pump 66dx40g1 parts diagram and verify your pump model number on the crankcase nameplate.
Locate – Find the valve plugs on the top and side of the brass manifold using the exploded layout.
Reference – Cross-check damaged O-rings, seals, or valve springs with callout numbers on the parts diagram list.
Connect/Route – Reinstall replacement seal packing stacks and valve kits into correct channels following diagram orientations.
Verify – Torque all brass manifold retaining bolts evenly to 125 in-lbs according to specified cross-pattern guidelines.
Troubleshoot – Check for oil or water leaks around the manifold seam during initial low-pressure runup testing.