Case IH 1020 Header Parts Diagram: 2026 Repair
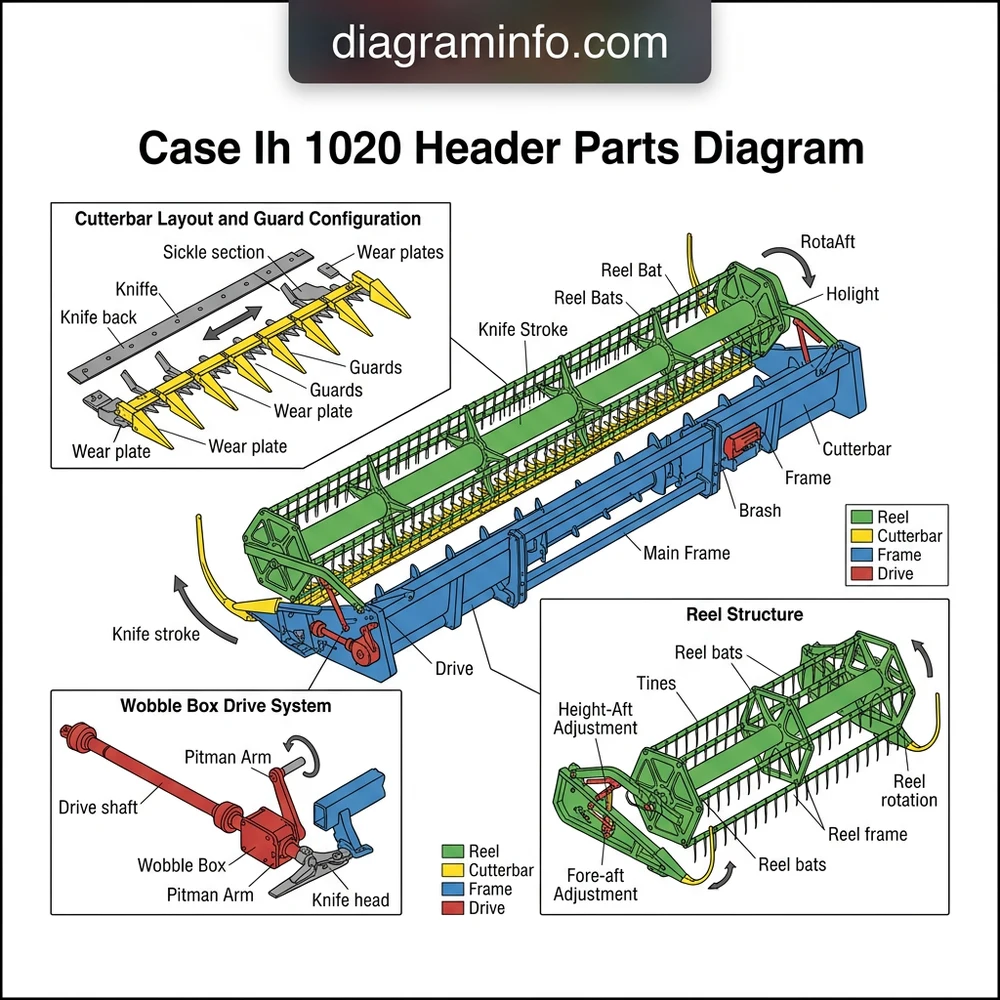
The Case IH 1020 header parts diagram details the flex cutterbar assembly, wobble box drive layout, dual auger fingers, and hydraulic reel drive system. It maps mechanical drive belts, cutterbar skid shoes, tension springs, and floor section arm linkages, allowing precise alignment, knife section replacement, and drive belt tensioning.
📌 Key Takeaways
- Wobble box mounting bolts require torque verification to 145 lb-ft to prevent drive housing fatigue.
- Flex cutterbar floor spring tension configuration determines ground pressure and flotation accuracy.
- Auger finger guide blocks and plastic bushings are primary wear points requiring annual clearance checks.
- Sickle drive belt spring length must match exact manufacturer specifications to avoid slippage.
- Proper hydraulic reel motor hose routing prevents pinch point damage during full vertical header travel.
The Case IH 1020 flexible grain header remains a gold standard for harvesting soybeans, legumes, and small grains due to its responsive cutterbar terrain tracking and durable drive architecture. Maintaining peak field throughput requires a complete structural and mechanical understanding of its internal assemblies. A comprehensive case ih 1020 header parts diagram serves as a vital technical roadmap, illustrating how the flex cutterbar, pick-up reel, cross auger, and drive systems function as a unified harvesting unit. Whether you are replacing worn sickle guards, rebuilding a failed wobble box drive, or adjusting float spring tension, referencing exact OEM schematics ensures correct component alignment, proper fastener torque, and maximum operating efficiency across all platform widths.
Case IH 1020 Header Parts Diagram: Structural Component Breakdown
Analyzing the overall case ih 1020 header parts diagram requires breaking down the platform into primary mechanical sub-assemblies. The platform framework consists of a heavy-duty steel beam spine supporting the float linkage arms, hydraulic reel lift cylinders, and main auger trough. Operating widths range from 15 feet to 30 feet, with structural bracing adjustments implemented depending on frame length.
Sickle section hardware (Grade 8 hex bolts): 12–14 ft-lbs (16–19 Nm). Knife drive head mounting bolts: 65–75 ft-lbs (88–101 Nm). Main wobble box frame housing bolts: 110–120 ft-lbs (149–163 Nm). Auger finger clearance to floor: 3/8 in. to 1/2 in. (9.5 mm to 12.7 mm).
The table below provides a detailed structural reference for key components mapped in standard Case IH 1020 schematic layouts, including primary service intervals and OEM specification standards.
| Sub-System | Diagram Reference / Component | OEM Part / Spec Identifier | Mechanical Function & Specs |
|---|---|---|---|
| Cutterbar Assembly | Sickle Guards & Hold-Downs | 130006C2 / 1956798C1 | Provides clean scissor shearing action against knife sections; requires 0.010–0.030″ hold-down gap. |
| Drive Transmission | Wobble Box Assembly | 1327318C91 / 190400C92 | Converts rotational shaft input to 3-inch linear knife stroke at 500–600 SPM. |
| Feeder System | 20-Inch Feed Auger | 1307613C91 (1.5″ Hex Drive) | Conveys cut crop into combine feeder house; equipped with adjustable spring slip clutch. |
| Reel Assembly | Teardrop Reel Drive Motor | 131846C1 (Orbital Hydraulic) | Drives 5 or 6-bat reel speed dynamically via variable flow valve; operates up to 2200 PSI. |
| Float Mechanism | Flex Arms & Poly Skids | 1307432C2 / High-Density Poly | Allows 6 inches of vertical flex range to follow uneven field terrain without soil scoop. |
Reading the Case IH 1020 Header Parts Diagram Step-by-Step
Interpreting an OEM exploded view drawing requires a structured approach to ensure correct teardown and reassembly sequence. Visual schematics use numerical callouts tied directly to an indexed parts list, depicting hardware, shims, bearings, and structural casting orientation.
Deciphering Exploded View Assemblies and Fastener Callouts
In a typical case ih 1020 header parts diagram, sub-assemblies are drawn detached along central axis lines. Key callout numbers point directly to individual components. For instance, in the wobble box mounting diagram, the primary housing casting is surrounded by split shims, needle bearings, output pitman arms, and mounting grade-8 bolts. When reassembling, follow the axis lines inward toward the main casting to ensure seal lips point toward oil cavities and lock washers are installed on the tension side of structural hardware.
Navigating Serial Number Breaks and Production Year Changes
Case IH manufactured the 1020 header over several decades (1988 through the early 2000s), resulting in key mechanical design revisions. Early models (pre-1995) utilized traditional single-bar sickle drives and cast steel hold-downs, while later models (post-1998) featured heavy-duty SCH Schumacher cutterbar conversions, updated poly skid shoes, and quick-attach header hookups. Always verify your header’s frame serial number (located on the rear left beam near the feeder house opening) against the parts blueprint. For detailed header setup matching your combine feeder house, refer to our guide on Case IH axial-flow combine feeder house adjustments.
Mapping Hydraulic Lines and Mechanical Drive Chains
Hydraulic schematics within the blueprint outline the reel lift and reel fore/aft circuits. Dual hydraulic cylinders on the left and right lift arms operate on a master-slave hydraulic loop to ensure parallel reel lifting. When inspecting drive chain configurations, locate the auger drive tightener sprocket and primary countershaft layout. The main countershaft transfers PTO power from the feeder house floor drive to the left-hand main jackshaft via heavy #80 drive chain.
Before performing service beneath a Case IH 1020 header, always lower the header safety stops onto the feeder house cylinders and lock the cutterbar flex arms in the rigid position using the factory lock pin channels. Never rely solely on hydraulic pressure to hold the reel or header raised during cutterbar maintenance.
Understanding Drive Layout and Flex System Configuration
The performance of the Case IH 1020 relies on two crucial systems working in sync: the mechanical wobble box knife drive and the flexible floor float control architecture.
If your standard Case IH wobble box experiences recurring housing fractures or excessive vibration in heavy canopy soybeans, evaluate converting to a planetary knife drive. For operators upgrading to a high-speed knife drive, see our detailed guide on Schumacher cutterbar conversion procedures.
Standard Mechanical Wobble Box vs. Schumacher Knife Drive Layout
The standard OEM wobble box uses an eccentric shaft layout to translate rotary motion from the drive belt pulley into vertical and horizontal knife arm oscillations. The schematic details internal needle bearings, tapered roller bearings, and an internal oil bath requiring 80W-90 gear lubricant. The output arm connects to the sickle bar head using a heavy pin bushing. In contrast, late-model planetary drive configurations eliminate lateral push-rod movement entirely, producing a pure linear stroke that reduces cutterbar fatigue and vibration.
Flex Arm Geometry and Float Control Linkage System
The flex system relies on a series of spring-loaded support arms spaced along the underside of the header floor frame. Each arm connects to a ground-facing poly skid shoe and a lateral spring adjustment rod behind the main frame beam. Turning the rear adjustment nuts alters spring compression, increasing or decreasing the weight carried by the ground skids:
- Tightening Float Springs: Decreases ground contact pressure, enabling the cutterbar to “float” easily over soft soil and mud without pushing dirt.
- Loosening Float Springs: Increases ground contact pressure, preventing the cutterbar from bouncing or riding over low-lying crop pods in firm ground conditions.
- Locking Rigid Pins: Converts the flexible floor into a rigid platform for harvesting standing wheat, barley, or oats.
Properly adjusting header float sensitivity requires matching settings with Case IH header height control sensors calibration specs to ensure automatic potentiometer sensors send accurate voltage signals back to the combine cab module.
Troubleshooting Mechanical Failures with the Case IH 1020 Blueprint
When mechanical breakdowns occur in the field, referencing the case ih 1020 header parts diagram aids in rapid root-cause diagnosis and replacement part selection. Below are technical diagnostic pathways for common header failures.
Sickle Section Shearing and Knife Head Fatigue Breaks
If the cutterbar consistently shears knife head bolts or snaps sections near the wobble box connection, consult the knife drive alignment schematic. Misaligned hold-down clips cause binding along the knife back channel. Use a dial indicator or alignment bar to check the entire cutterbar run:
- Verify hold-down lip clearance is set between 0.010 and 0.030 inches along every guard section.
- Inspect wear plates under the sickle bar for step-wear pattern grooves; replace plates if lip thickness drops below 0.120 inches.
- Check the wobble box output arm alignment relative to the knife head connection pin. Off-center drive linkage causes severe fatigue bending on every stroke stroke cycle.
Auger Drive Slip Clutch Slipping and Feed Choking
When heavy soybean windrows cause the center feed auger to stop while the drive belt continues turning, the auger slip clutch requires inspection. Locate the auger drive sprocket schematic on the left end-panel layout:
- Inspect the friction discs inside the clutch hub; minimum disc thickness specification is 0.125 inches (3.18 mm).
- Measure spring compression height across all tension bolts. Standard factory spring length when compressed is 1.31 inches (33.3 mm).
- Ensure retractable auger finger guide plastic bushings are intact. Broken guide bushings cause internal retractable fingers to bind, locking the auger shaft.
Uneven Flex Response and Cutterbar Digging
If one section of the cutterbar digs into the ground while adjacent sections lift correctly, refer to the flex arm pivot schematic. Check for bound pivot pin bushings or broken leaf-spring linkages behind the frame channel. Inspect poly skid shoes for missing carriage bolts or severe gouges that create localized drag against the ground surface.
Case IH 1020 Grain Header Parts Diagram FAQ
How do I identify the correct wobble box configuration on a Case IH 1020 diagram?
Identify your wobble box type by checking the input pulley placement and mounting flange orientation on the left side of the header. Standard OEM boxes feature a vertical mounting flange with an oil fill plug on top and a horizontal pitman arm link. Late-model or aftermarket planetary drives feature a fully enclosed inline box mounted directly in line with the cutterbar plane without external rocker arms.
What are the standard torque specifications for Case IH 1020 sickle section bolts?
Grade 8 smooth or serrated flange nuts used on Case IH 1020 sickle sections should be torqued to 12–14 ft-lbs (16–19 Nm). Over-torquing can distort the soft steel knife bar strip, leading to binding against guard channels, while under-torquing allows vibration to loosen section hardware during high-frequency operation.
How does the flex cutterbar float system register on the schematic layout?
On the parts diagram, the float system is illustrated under the lower frame assembly section. It comprises individual flex arms, torsion springs, pivot pins, adjusting eye-bolts, and ground skid shoes. The blueprint shows how tightening the rear spring tension nuts relieves cutterbar weight on the ground skid shoes, allowing the bar to flex through its 6-inch vertical operating window.
Where can I find the serial number tag on my Case IH 1020 header to match parts diagrams?
The serial number plate is riveted to the rear vertical sheet-metal beam of the main header frame, located on the left-hand side near the feeder house adapter frame opening. Always cross-reference this serial number when ordering drive belts, wobble box components, and hydraulic reel motors, as mid-series production changes alter part numbers.
What is the difference between early and late style reel drive hydraulic configurations?
Early-style Case IH 1020 headers utilized a standard open-loop hydraulic drive line fed by the combine’s hydraulic pump, featuring hard steel hydraulic lines running along the upper main frame beam. Late-style configurations incorporate quick-disconnect multi-coupliers, upgraded orbital drive motors with integrated cross-over relief valves, and reinforced flexible rubber lines designed to accommodate higher flow rates and fore/aft reel adjustments without hose kinking.