GM Rochester 2 Jet Carburetor Diagram: Troubleshooting 2026
A Rochester 2 Jet carburetor diagram details the air horn, main body, float assembly, power valve, and throttle body. Standard float level setting is typically 1/4 inch, with air horn screws tightened to a torque spec of 30-35 inch-pounds. Adjust idle mixture screws 1.5 turns out from seated for initial startup.
📌 Key Takeaways
- Standard air horn screw torque spec is 30-35 inch-pounds to prevent casting warpage.
- Differentiate 2GC (choke on carburetor) from 2GV (well-mounted choke thermostatic spring) models.
- Vacuum leaks from cracked base gaskets can disrupt air-fuel ratios and trigger an OBD-II diagnostic code on converted engines.
- The accelerator pump cup soft seal is the most frequent wear point causing off-idle hesitation.
- Basic rebuilds are ideal for DIY, but eroded throttle shaft bores require professional bushing installation.
The Rochester 2 Jet carburetor—encompassing the classic 2G, 2GC, and 2GV variants—served as the core two-barrel fuel metering standard for General Motors passenger vehicles, light trucks, and marine applications from 1955 through the late 1970s. Engine owners and professional mechanics working on vintage V8 and V6 platforms rely on precision schematic references to service these mechanical fuel units. Utilizing a full technical rochester 2 jet carburetor diagram allows you to systematically trace internal fuel passages, calibrate float height parameters, troubleshoot vacuum enrichment circuits, and ensure the complete air-fuel circuit maintains stoichiometric balance under varying engine loads.


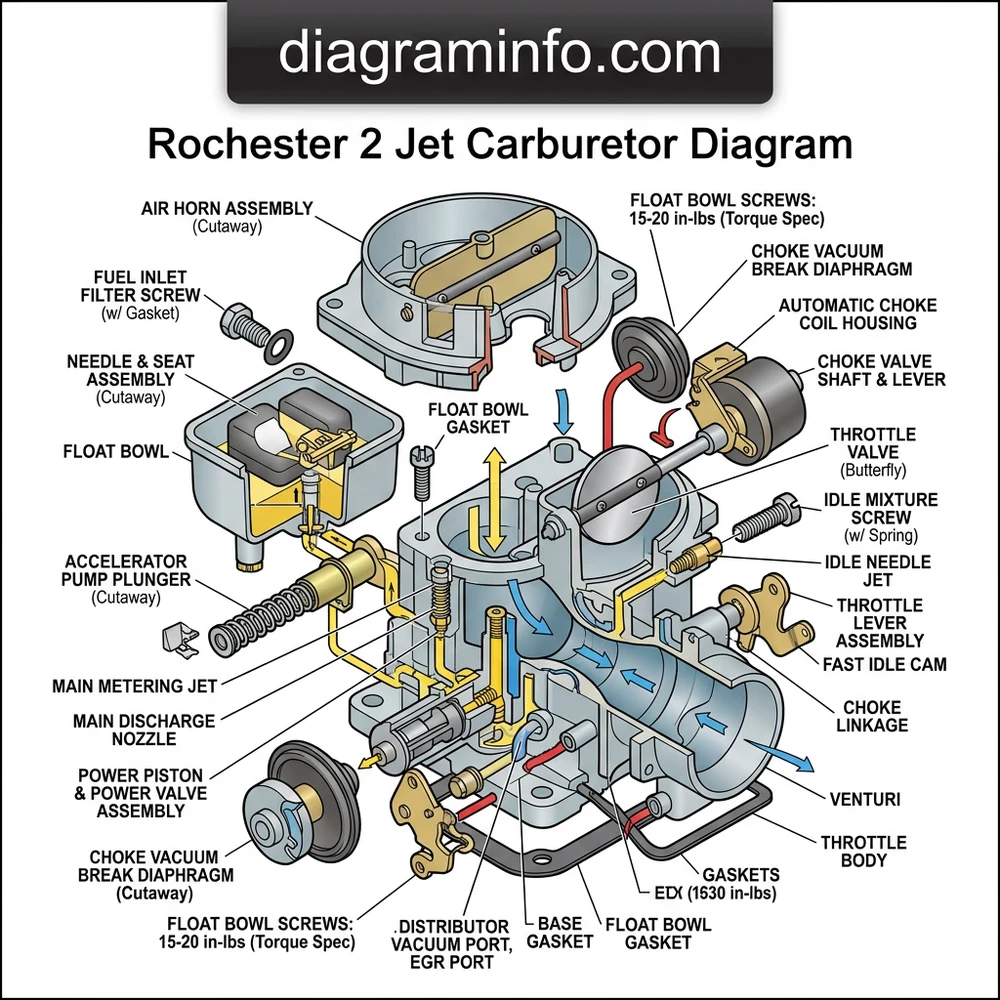
Rochester 2 Jet Carburetor Diagram Component Identification and Assembly


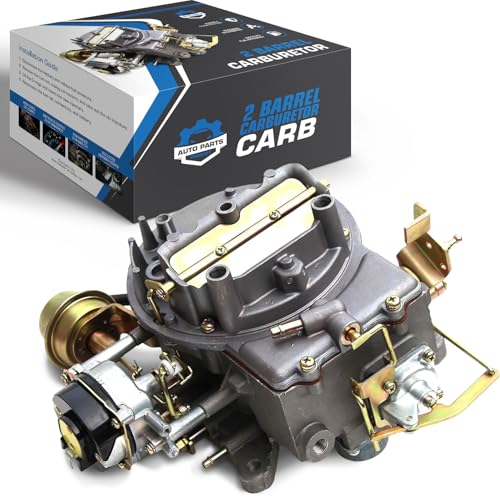
The architecture of the Rochester 2 Jet series is divided into three primary cast housings: the air horn (top assembly), the main body (bowl assembly), and the throttle body (base plate assembly). Each casting isolates vital fuel metering and air management components sealed by precision cut gaskets. Analyzing a rochester 2 jet carburetor diagram reveals the exact alignment and mechanical interface of these individual structural elements.
The upper air horn casting houses the air cleaner stud boss, fuel inlet filter nut, choke plate shaft, pump lever, and vacuum break diaphragm. Positioned underneath the air horn assembly is the internal float mechanism, suspended via a stainless steel hinge pin inserted into designated casting stanchions. The float regulates the incoming fuel supply by pressing a viton-tipped needle against a replaceable brass seat.
The main body casting contains the central fuel bowl, dual venturi clusters, main metering jets, accelerator pump well, and the spring-loaded power piston assembly. Positioned directly at the bottom of the main body, the cast-iron or heavy aluminum throttle body contains the brass throttle plates, throttle shaft, idle bypass passages, and dual adjustable needle valves used to trim idle air-fuel ratio delivery.
| Component Name | Factory Specification / Thread Size | Recommended Torque Spec |
|---|---|---|
| Air Horn Retaining Screws (8 Outer/Inner) | #10-32 UNC Machine Screws | 25 – 30 in-lbs (2.8 – 3.4 Nm) |
| Fuel Inlet Filter Nut | 1-” x 20 Straight Thread / Brass Washers | 18 – 22 ft-lbs (24 – 30 Nm) |
| Main Metering Jets (Dual) | 1/4″-32 Thread (Sizes #50 to #74) | 18 – 22 in-lbs (2.0 – 2.5 Nm) |
| Throttle Body to Main Body Screws | 1/4″-20 UNC Countersunk Screws | 45 – 55 in-lbs (5.1 – 6.2 Nm) |
| Carburetor Mounting Flange Nuts | 5/16″-18 Stud Fasteners | 12 – 15 ft-lbs (16 – 20 Nm) |
Factory dry float level for standard Rochester 2GC applications is typically set at 21/32 inches measured from the air horn gasket surface to the toe of the float. Always verify against specific engine code stamping numbers on the float bowl rim, as marine and heavy-duty truck specs vary between 1/2 inch and 23/32 inches.
Functional Systems in Rochester 2G, 2GC, and 2GV Carburetors


Understanding how air and liquid fuel move through the schematic paths of the Rochester 2 Jet demands analyzing its five distinct operating circuits: the float system, idle enrichment system, main metering system, power enrichment system, and pump system.
1. Float System Operations
Fuel enters the carburetor through the inlet filter nut, flowing past the needle and seat directly into the bowl chamber. The buoyed float rises as the chamber fills, pushing the needle into the valve seat when the fuel level reaches calibrated height. Unrestricted flow maintaining 4.5 to 6.5 PSI from the mechanical fuel pump prevents fuel starvation under full throttle while keeping the needle seated during idle.


2. Idle and Off-Idle Metering Circuits


At idle engine speeds, throttle plates remain almost completely closed, producing high vacuum inside the manifold beneath the base plate. Vacuum draws raw fuel from the main bowl down through idle pickup tubes inserted into the venturi cluster. This liquid fuel mixes with fresh air entering from primary idle air bleeds. The resulting emulsion travels down channels inside the main body casting, exiting through adjustable idle needle holes situated below the throttle valves.
3. Main Metering and Venturi Booster Systems
As throttle linkage opens past off-idle transition slots, high airflow velocity moving through the primary venturi creates a low-pressure area across the venturi cluster nozzles. Atmospheric pressure pushing on the top of the fuel bowl forces fuel down through the primary brass main jets, up through vertical main wells, and into the booster venturi outlets where it atomizes into the main intake airstream.
Unlike later electronic fuel injection setups managed by a central digital system, the Rochester 2 Jet relies strictly on mechanical differential pressure. For deeper insight into mechanical vs digital air-fuel management, refer to our comprehensive technical manual on ignition system wiring diagrams and retrofitting distributor timing curves.
4. Power Enrichment Valve Circuit


Under heavy acceleration or high engine load, manifold vacuum drops below 6 to 8 inches of mercury (in-Hg). A mechanical spring mounted above the power piston overcomes this reduced vacuum, pushing the power piston downward. The lower tip of the piston unseats the spring-loaded power valve ball inside the bottom of the float bowl. This opens a supplemental fuel channel bypass, enriching the main metering mixture by 20% to 25% to protect pistons from detonation and lean-burn damage.


5. Accelerator Pump and Choke Heat Controls
Rapid opening of the throttle causes a brief drop in air velocity, creating a temporary lean condition. To counteract this, a leather or synthetic cup accelerator pump plunger mechanically connected to the throttle lever forces a solid shot of liquid fuel through internal check valves directly out of the pump cluster nozzles. Engine thermal regulation is managed via the choke system. Model 2G relies on manual choke control, 2GC utilizes an air-horn-mounted thermostatic coil heated by hot manifold air or engine manifold coolant flow heat crossover channels, while 2GV uses a remote choke spring mounted directly to the intake manifold floor.
Isolating Carburetor Malfunctions from Engine Mechanical Faults



Diagnostic troubleshooting requires determining whether performance degradation stems directly from fuel delivery issues mapped on your rochester 2 jet carburetor diagram, or from underlying engine mechanical wear. Because classic carbureted engines lack an onboard computer engine diagnostic port, mechanics cannot pull a digital diagnostic code or scan for a illuminated dash illumination light when troubleshooting engine stumbles.
Excessive fuel delivery caused by a needle leak or stuck power piston will wash oil off cylinder walls, diluting crankcase lubricating oil. This reduces engine oil pressure and leads to severe main bearing wear. Always inspect dipstick oil viscosity and fuel odor when diagnosing persistent flooding conditions.
When an engine experiences unstable idle or severe bog, perform a systematically sequenced component check. High mileage vintage V8 engines frequently display symptoms that mimic carburetor failure but originate from internal mechanical components:
- Timing Chain Slack: A stretched timing chain changes valve timing relative to crankshaft position. Retarded valve timing reduces engine idle vacuum down to 10-12 in-Hg (standard baseline is 17-21 in-Hg). This reduced vacuum prevents the power piston from remaining fully retracted, causing the power valve to leak continuous excess fuel at idle.
- Intake Manifold Gasket Vacuum Leaks: Unmetered air entering through cracked manifold gaskets or dried base plate gaskets dilutes the idle air-fuel ratio. Adjusting idle mixture needles will yield no engine response when air bypasses the carburetor entirely.
- Fuel Dilution and Bearing Clearance: Persistent carb flooding dilutes engine oil, lowering warm engine oil pressure. If low pressure warnings appear, check whether raw gasoline is overflowing into the crankcase before replacing mechanical oil pumps.
- Blocked Coolant Passages: Thermostatic choke housings on 2GC models rely on continuous exhaust cross-over heat or engine coolant flow through heat riser plates. Restricted passages keep the choke plate partially closed, causing black smoke emissions and spark plug fouling.
If you are also diagnosing charging and auxiliary engine electrical systems on vintage GM machinery, review our technical guide regarding starter relay wiring diagrams to ensure stable cranking voltages during cold start choke tests.
Diagnostic Steps for Tuning and Rebuilding from the Rochester 2 Jet Carburetor Diagram
Performing a complete calibration or overhaul requires following organized teardown and specification procedures. Follow these step-by-step diagnostic instructions to restore accurate fuel metering using your structural diagram.
- Perform Float Height and Level Alignment: Invert the air horn assembly vertically with the gasket installed. Measure the vertical gap between the air horn gasket face and the bottom edge of the float pontoon. Bend the float arm brass tab gently until the dimension reaches exactly 21/32 inches. Turn the air horn right-side up to check float drop; adjust the rear float drop stop tab until total vertical float travel measures 1-3/4 inches.
- Inspect and Test Vacuum Power Piston Operation: Depress the power piston shaft down into its bore inside the air horn or cluster body, then release it. The piston must move completely free without binding or dragging on varnish deposits. Apply vacuum using a hand pump directly to the vacuum signal channel; the piston must pull fully upward and hold steady vacuum without leak-down.
- Set Static Idle Mixture Needle Baseline: Thread both brass idle mixture screws fully inward into the throttle body base plate until they lightly seat. Do not overtighten, or you will groove the needle tips and ruin the idle ports. Back each screw outward exactly 1.5 full turns counterclockwise to establish initial start-up calibration.
- Calibrate Accelerator Pump Stroke: Place the pump rod into the inner or outer hole of the throttle lever arm as designated by your engine build code. Measure total pump rod height from the top of the air horn ring down to the top of the pump stem with the throttle closed. Bend the offset bend in the pump rod to adjust height within +/- 1/64th inch of factory spec.
- Perform Dynamic Idle Tuning with Vacuum Gauge: Connect an analog vacuum gauge to an unswitched manifold vacuum port below the throttle plates. Warm the engine up to operating temperature so the choke plate stands completely vertical. With the engine idling in Neutral (or Park), adjust each idle mixture screw in 1/4-turn increments until you locate the peak vacuum reading on the gauge, then back out 1/8 turn rich.
For additional details on tracing primary vacuum circuits, electrical paths, and mechanical sensor integration across vintage engine bays, consult our guide on 3 wire alternator wiring diagrams.


Bridging Vintage Rochester 2G Systems to Modern ECU and OBD-II Diagnostics
While original Rochester two-barrel carburetors are completely mechanical, many classic car builders convert these platforms or integrate modern engine telemetry. Pre-1996 muscle cars and trucks do not feature factory OBD-II port connections or direct engine computer controls. Consequently, traditional engines cannot diagnostic code or trigger an illuminated check engine light when misfires occur.
To overcome this diagnostic gap when tuning a Rochester 2 Jet, technicians often temporarily install a wideband oxygen (O2) sensor in the exhaust collector paired with an aftermarket digital gauge. This setup provides real-time air-fuel ratio (AFR) data. At cruise speeds, a properly jetted Rochester 2 Jet should display 14.2:1 to 14.7:1 AFR. Under wide-open throttle (WOT), the mechanical power valve should enrich the mixture down to 12.5:1 to 12.8:1 AFR.
If you decide to replace the Rochester 2 Jet entirely with a modern standalone Throttle Body Injection (TBI) unit, a standalone engine ECU manages fuel injector pulse widths electronically. Modern electronic systems monitor coolant temperature sensors, throttle position, and MAP vacuum sensors to eliminate cold-start tuning quirks, allowing full diagnostic capabilities using modern handheld scan tools.
Rochester 2 Jet Carburetor Diagram Frequently Asked Questions
How do I identify whether I have a Rochester 2G, 2GC, or 2GV carburetor model?


The base model 2G utilizes a manual choke lever operated via an engine bay cable. The 2GC model features an automatic choke unit mounted directly on the side of the air horn casting, utilizing hot air tubes or an internal electric choke element. The 2GV model lacks an integral choke housing on the carburetor body, instead using a remote thermostatic choke spring mounted directly onto the intake manifold surface connected via a thin vertical steel rod.
What causes fuel to pour out of the venturi stack nozzles at idle?
Fuel discharging directly out of the venturi cluster at idle indicates high fuel bowl level or a unseated needle valve. Common root causes include dirt trapped between the viton needle tip and brass seat, excessive fuel pump pressure exceeding 6.5 PSI, a sunk float filled with fuel, or an improperly set float level adjusted too high. Check incoming fuel pressure with a mechanical gauge before rebuilding the unit.
What is the correct torque spec for assembling the Rochester 2 Jet castings?
The top air horn assembly machine screws require a torque spec of 25 to 30 in-lbs applied in an alternating cross-pattern to prevent warping the thin aluminum casting. Main body to throttle base plate countersunk screws should be torqued to 45 to 55 in-lbs. The intake manifold flange mounting nuts require 12 to 15 ft-lbs of torque to seal the base gasket without cracking the cast iron flange ears.
Can a worn timing chain cause fuel delivery symptoms mistaken for a carburetor defect?
Yes. Excessive slack in a worn engine timing chain alters camshaft indexing relative to the crankshaft, lowering baseline engine vacuum. Because the internal power piston in a Rochester 2 Jet relies on manifold vacuum to stay pulled upward in its bore, low engine vacuum allows the spring to push the piston down prematurely. This opens the power valve constantly, dumping raw fuel into the engine at idle and mimicking a blown carburetor internal seal.
Why does my engine stumble upon pressing the gas pedal despite a new pump cup?
If acceleration stumble occurs after installing a fresh accelerator pump cup, verify that the internal steel check ball is present inside the pump well bottom. Without the lower intake check ball and top discharge cluster needle installed, pressing the throttle forces fuel backward into the float bowl rather than spraying out the nozzle cluster ports into the venturi streams.
Step-by-Step Guide to Understanding the Rochester 2 Jet Carburetor Diagram
Identify – Determine your exact model variation (2G, 2GC, or 2GV) using the stamped triangular tag or air horn casting number.
Locate – Reference the diagram to locate top air horn screws, choke linkages, and vacuum lines before starting disassembly.
Reference – Use the exploded schematic to remove internal components sequentially, noting small check ball locations in the pump well.
Connect/Route – Reassemble internal circuits and route throttle, choke, and vacuum lines according to diagram pathways.
Verify – Set float height to 1/4 inch and tighten air horn fasteners to the recommended torque spec of 30-35 inch-pounds.
Troubleshoot – Adjust idle mixture screws 1.5 turns out; if rough idling persists, check vacuum ports with a pressure gauge.