Replacement Parts Scorch Torch Assembly Diagram: Installation Setup 2026
The replacement parts scorch torch assembly diagram details the direct integration between the high-temp burner assembly, fuel solenoid, and HVAC flame sensor. Connected upstream of the blower motor and heat exchanger circuit, it requires 24VAC control power, R-410A thermal isolation clearances, and an exact 1/8-inch spark gap for reliable ignition.
📌 Key Takeaways
- Maintain an exact 1/8-inch (3.18 mm) gap between the spark electrode and torch burner head.
- Ensure flame sensor microamp readings register between 2.0 and 5.0 µA DC during active burner operation.
- Always disconnect 120V main power and 24V control power before replacing torch assembly leads.
- Misrouting high-voltage igniter wires near low-voltage blower motor leads causes severe electrical interference.
- Gas solenoid coils require 24VAC input; verify manifold pressure at 3.5 in. W.C. for natural gas setups.
Precision servicing of auxiliary thermal heating and ignition units requires an exact interpretation of the replacement parts scorch torch assembly diagram. In heavy-duty automotive, mobile HVAC, and industrial air handler environments, the Scorch Torch sub-assembly functions as an auxiliary thermal generator or flame-assisted defrost booster. This unit works in tandem with key climate components, including the heat exchanger, evaporator coil, and main blower motor. Navigating the manufacturer schematic ensures field technicians maintain OEM electrical tolerances, proper fuel/air mixture ratios, and hermetic fluid isolation. The following guide provides a comprehensive breakdown of assembly schematics, component specs, and step-by-step field overhaul procedures.


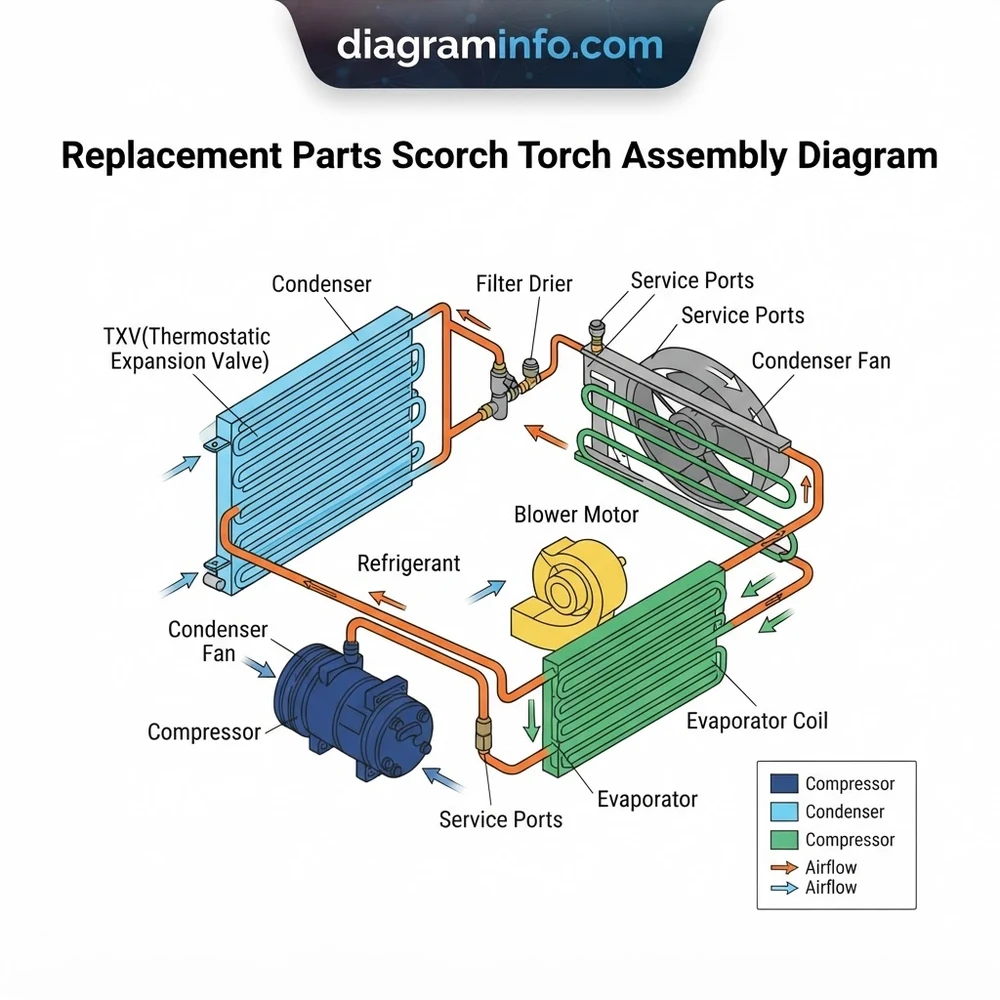
Understanding the Replacement Parts Scorch Torch Assembly Diagram

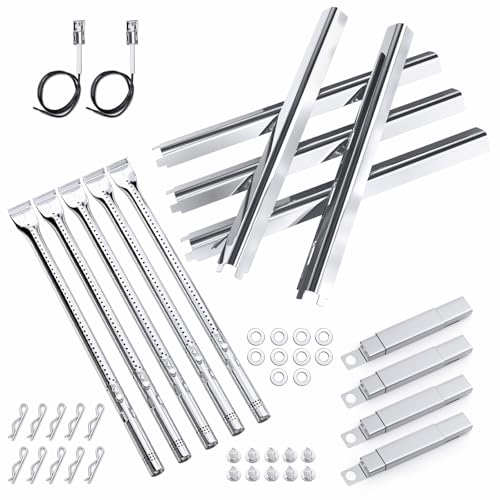

According to OEM technical specifications, the auxiliary scorch torch mechanism operates within high-thermal zones adjacent to the primary heat exchanger. The assembly schematic delineates critical mechanical joints, high-voltage ignition leads, fuel-metering solenoid valves, and pneumatic sensing lines. Recognizing how these sub-components interface with the broader HVAC loop—specifically the compressor circuit, condenser coil, and air handler housing—is vital before initiating teardown.
When reviewing the replacement parts scorch torch assembly diagram, technicians must identify the dual-stage ignition module, stainless steel combustion nozzle, and internal flame-rectification rod. These elements are co-located within the burner tube to ensure instantaneous thermal output without inducing localized hot spots on the surrounding evaporator fins or return duct insulation lining.
| Diagram Reference # | Component Description | OEM Specification / Voltage | Functional Interface |
|---|---|---|---|
| ST-101 | Combustion Burner Tube Assembly | 304 Stainless Steel / 1200°F Rating | Mounts directly into primary air handler plenum |
| ST-102 | Direct Spark Ignition Electrode | 15kV Peak / Orange Silicone Wire Lead | Interfaces with master ignition controller board |
| ST-103 | Fuel Control Solenoid Valve | 24VAC Nominal / 0.35A Draw (Blue/White) | Controls liquid/gas feed to nozzle assembly |
| ST-104 | High-Temperature Cutoff Switch | 450°F Auto-Reset Limit / NC Contact | Inline with blower motor interlock wiring |
| ST-105 | Flame Rectification Sensor Rod | 2.0 – 6.0 Microamps DC Signal | Feeds flame validation signal to control board |
Always check for harness revision codes on the Scorch Torch assembly graphic before ordering replacement leads. Model years 2021 and newer utilize a 6-pin Weather-Pack connector, whereas earlier revisions feature spade-terminal jumper blocks on the main air handler frame.
Compressor and Condenser Circuitry Integration
Although the Scorch Torch functions primarily in a heating or thermal boost capacity, the control loop communicates directly with the compressor clutch relay and the outdoor condenser fan circuit. When the Scorch Torch initiates a high-output defrost cycle, the control board triggers a temporary lock-out signal to the refrigeration compressor. This prevents liquid refrigerant slugging back through the suction line into the compressor crankcase while heat is directed across the evaporator core.
Evaporator and Heat Exchanger Core Components


The thermal discharge from the Scorch Torch nozzle is directed downstream toward the heat exchanger face. Airflow drawn from the return duct passes over the heat exchanger fins, picking up latent BTUs generated by the burner unit. Concurrently, the evaporator coil upstream must remain isolated from direct flame impingement. The replacement parts scorch torch assembly diagram indicates exact spatial clearances—typically a minimum 4.5-inch offset—between the tip of the burner cone and the aluminum evaporator face.
Air Handler Blower Motor and Return Duct Mechanics
Proper air volume across the Scorch Torch heat shield is maintained by the variable-speed ECM blower motor. If static pressure in the return duct spikes due to a clogged air filter or damaged ductwork, the reduction in CFM can cause the Scorch Torch burner ambient temperature to spike rapidly. The air handler’s differential pressure switch continuously monitors velocity pressure across the return duct, dropping out the Scorch Torch solenoid valve if static pressure falls below 0.20 in. w.g.


Replacement Parts Scorch Torch Assembly Diagram Installation Guide


Rebuilding or installing an auxiliary Scorch Torch module requires strict adherence to physical clearances, electrical wire routing, and mechanical fastener torque values. Below are the required field conditions, tool specifications, and safety guidelines for completing this procedure.
Estimated Time: 2.5 to 3.5 Hours
Required Tools: 1/4″ & 3/8″ Drive Torque Wrenches, Digital Multimeter (True-RMS with Microamp scale), Refrigerant Gauge Manifold, Flare Nut Wrenches (10mm to 19mm), Wire Strippers/Crimpers, Calibrated Gas Leak Detector.
Torque Specs: Burner Mount Bolts (85 in-lbs), Gas Solenoid Flare Connections (18 ft-lbs), Electrical Terminal Screws (12 in-lbs).
Disconnect all high-voltage power feeds (240VAC/480VAC) to the air handler unit before removing access panels. Verify that the system high-pressure refrigerant line is discharged or isolated according to EPA Section 608 guidelines if servicing adjacent evaporator tubing. Lockout/Tagout (LOTO) protocols must be enforced.
1. System Shutdown and Isolation


Turn off power at the main equipment breaker panel and apply Lockout/Tagout devices to the main disconnect. Shut off the auxiliary fuel feed valve to the Scorch Torch assembly. Using a digital multimeter, check for zero voltage across lines L1, L2, and the control board 24VAC control transformer leads inside the air handler electrical enclosure.
2. Accessing the Scorch Torch Burner Bay
Remove the six 5/16-inch sheet metal screws securing the lower access door on the air handler cabinet. Disconnect the return duct flex-connector if necessary to gain adequate clearance around the combustion chamber. Carefully peel back the foil-faced fiberglass insulation to expose the mounting flange indicated on the replacement parts scorch torch assembly diagram.


3. Removing Damaged Components and Disassembling the Module


Unplug the 6-pin Weather-Pack wiring harness connecting the ignition spark wire (Orange lead) and flame sensor rod (Yellow lead). Using a flare nut wrench, disconnect the hard fuel line from the inlet side of the fuel control solenoid valve (Item ST-103). Remove the four 10mm hex-head mounting bolts holding the Scorch Torch flange to the internal heat exchanger bulkhead. Slide the worn torch assembly out of the air handler housing.
4. Installing the Scorch Torch Assembly and Mounting Hardware
Inspect the replacement Scorch Torch assembly against the reference schematic to ensure all gaskets and ceramic insulators are installed correctly. Align the new burner tube with the heat exchanger intake port, ensuring the flame baffle points directly down the center axis of the chamber. Thread the four mounting bolts by hand to prevent cross-threading, then torque in a cross-pattern to 85 in-lbs using a 1/4-inch drive torque wrench.
5. Reconnecting Fuel Lines, Wiring Harnesses, and Sensor Loops
Reinstall the fuel supply pipe to the solenoid valve inlet. Torque the brass flare fitting to 18 ft-lbs using two wrenches to back-wrench the valve body. Reattach the 6-pin Weather-Pack wiring block. Route the high-voltage ignition wire away from sharp metal edges, securing it with high-temperature P-clips as shown in the diagram wiring pathway detail. Reconnect the 24VAC safety limit switch terminals (Red and Black wires).
6. System Pressure Check, Electrical Verification, and Test Firing
Apply 15 PSI of nitrogen or utilize an electronic gas leak detector at all fuel line flare joints to confirm bubble-tight integrity. Restore electrical power to the air handler and set the system thermostat to call for auxiliary heat. Observe the blower motor starting sequence—the ECM blower motor must establish baseline air pressure through the return duct before the ignition board activates the Scorch Torch spark module. Confirm a stable flame signal of 2.0 to 6.0 microamps DC on your multimeter once ignition occurs.
Troubleshooting Systems via the Replacement Parts Scorch Torch Diagram


System failures within the auxiliary scorch torch loop usually present as ignition lockouts, insufficient thermal rise, or unexpected system trips on high-limit switches. Utilizing the replacement parts scorch torch assembly diagram alongside structured electrical and mechanical testing accelerates root-cause isolation.
Refrigerant Leak Diagnostics and Evaporator Pressure Drops
If the Scorch Torch generates excessive heat during a defrost sequence, radiant thermal output can cause rapid pressure spikes in the evaporator coil. Check system operating parameters using a digital gauge manifold attached to the suction and liquid service valves near the compressor unit.


- High Evaporator Pressure during Defrost: Indicates the Scorch Torch is running beyond calibrated duration, risking thermal overload at the compressor suction port. Check the defrost termination sensor attached to the heat exchanger outlet.
- Low Refrigerant Charge Symptoms: If the evaporator is undercharged, subcooling at the condenser drops below 5°F, causing frost buildup that forces the Scorch Torch to cycle continuously. Leak test all braze joints around the air handler.
- Solenoid Cycling Faults: Verify 24VAC control signal across the solenoid terminals. If voltage drops below 21.6VAC during burner engagement, inspect the control transformer and supply wiring for high resistance.
Blower Motor Overheating and Heat Exchanger Thermal Airflow Faults
When the high-temperature cutoff switch (ST-104) trips open, the Scorch Torch fuel solenoid immediately drops out while the blower motor continues running at maximum RPM. Refer to the diagnostic matrix below to trace airflow and electrical faults across the air handler and return duct network.
| Symptom | Probable Root Cause | Diagnostic Test Procedure | Corrective Field Action |
|---|---|---|---|
| No spark during ignition sequence | Cracked ceramic insulator on electrode (ST-102) | Check continuity between electrode wire terminal and ground frame | Replace spark electrode assembly; gap tip to 0.125 inches |
| Flame establishes then drops out after 3 seconds | Oxidized flame sensor rod (ST-105) or poor ground | Measure microamp DC current inline with sensor wire during firing | Clean rod with emery cloth or replace sensor; verify control board ground wire |
| High limit switch trips within 60 seconds | Low airflow from blower motor or blocked return duct | Measure static pressure in plenum using a digital manometer | Clean blower wheel, replace MERV filter, or clear obstructions in return duct work |
| Compressor liquid floodback post-defrost | Stuck condenser fan relay or shorted defrost control lead | Verify condenser fan operates when Scorch Torch drops out of heat mode | Replace defrost interface board or sticky mechanical relay contacts |
Replacement Parts Scorch Torch Assembly Diagram FAQs
How do I match part numbers on the Scorch Torch assembly schematic?
Locate the callout bubble numbers on your physical paper or digital schematic and cross-reference them with the legend table printed at the base of the drawing. OEM parts utilize a prefix corresponding to the burner frame size (e.g., ST-100 series for standard air handlers, ST-200 for heavy equipment commercial units). Always cross-check the revision suffix letter (Rev A, B, or C) printed on the air handler data plate before finalizing component orders.
What electrical tolerances are expected across the blower motor terminals?
When operating in tandem with the Scorch Torch assembly, variable-speed ECM blower motors expect a constant supply voltage of 208–230VAC single-phase across lines L1 and L2 (±10%). Control signals entering the motor interface board from the thermostat or master HVAC controller should read 24VAC across the G terminal during call-for-fan operations. Winding resistance across motor terminals T1-T2, T2-T3, and T1-T3 should be balanced within 0.5 ohms on an unpowered motor disconnect test.
Can I adapt a Scorch Torch unit to non-standard return duct setups?
Adapting the Scorch Torch to custom or retrofitted return duct configurations requires maintaining the original static pressure envelope. According to manufacturer guidelines, retrofits must maintain a minimum uniform velocity profile across the heat exchanger face. Installing turning vanes or transitions within 24 inches upstream of the air handler intake is mandatory if the ductwork makes a 90-degree bend right at the return collar flange.
What safety protocols govern refrigerant recovery during heat exchanger swaps?
If servicing the Scorch Torch requires unbolting or repositioning the adjacent evaporator coil, technicians must recover all system refrigerant into an EPA-certified recovery cylinder using a dedicated recovery unit. Never vent R-134a, R-410A, or R-1234yf to the atmosphere. Evacuate the sealed refrigerant system down to at least 500 microns before recharging by weight according to the data plate posted on the outdoor condenser cabinet.
Why is proper torque critical on condenser line flare fittings and torch fuel lines?
Improperly torqued flare fittings on gas fuel feeds or high-pressure refrigerant lines are the primary cause of field failures in high-vibration equipment applications. Under-torquing leads to micro-leaks caused by joint flexing during compressor startup cycles or air handler vibration. Over-torquing stretches brass flare nuts, splitting the copper flare seat and causing catastrophic pressure loss or fuel leakage into the burner plenum area. Always use calibrated torque wrenches set to manufacturer-specified foot-pound values.
Step-by-Step Guide to Understanding the Replacement Parts Scorch Torch Assembly Diagram
Identify – Identify all burner, igniter, and wiring components on the replacement parts scorch torch assembly diagram.
Locate – Locate the flame sensor, spark electrode, and gas control valve within the furnace unit housing.
Reference – Reference the diagram wire color codes and pin configurations before disconnecting any existing electrical connections.
Connect/Route – Route replacement wiring harnesses away from high-temperature burner surfaces and torque mounting fasteners to 25 in-lbs.
Verify – Verify spark electrode gap to 1/8 inch and confirm 24VAC control signal across the gas valve terminals.
Troubleshoot – Troubleshoot unverified burner ignition by testing flame sensor microamp DC output and checking blower motor interlock continuity.