Tweco MIG Gun Parts Diagram: Component Breakdown 2026
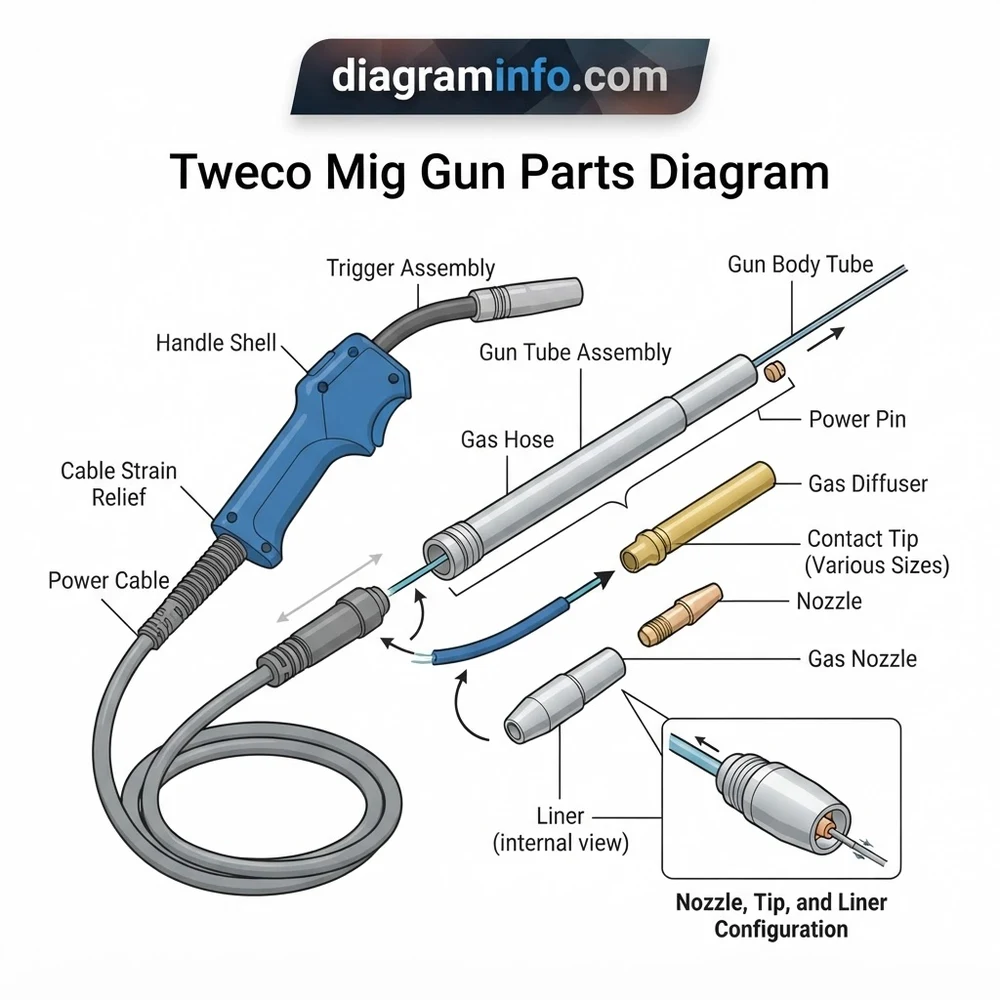
A Tweco MIG gun parts diagram illustrates the internal structure and component layout of the torch assembly. Key components include the gas nozzle, contact tip, diffuser, swan neck (conductor tube), trigger switch, internal wire conduit liner, power cable assembly, and Euro/Tweco rear machine connector. Understanding this system ensures proper gas flow, smooth wire feeding, and electrical continuity.
📌 Key Takeaways
- Contact tips and diffusers use coarse or fine copper threading depending on the Tweco series rating.
- Liner sizing must match exact wire diameter (.035″ or .045″) to prevent wire chattering and birdnesting.
- Gas diffuser ports must remain free of spatter to maintain laminar shielding gas flow configuration.
- Worn conductor tube insulators are the primary cause of internal electrical shorting to the gun handle.
- Replace contact tips when internal bore wear exceeds 0.010 inches over nominal wire diameter.
Understanding a Tweco MIG gun parts diagram is essential for maintaining arc stability, ensuring precise wire feeding, and replacing consumable components in industrial welding operations. Tweco air-cooled MIG guns—ranging from light-duty Mini-Mark and No. 1 series up to heavy-duty Spray Master and No. 4 models—utilize modular construction designed for high-duty-cycle performance. Interpreting these schematics correctly allows welding technicians and maintenance personnel to quickly identify worn contact tips, damaged gas diffusers, degraded conduits, and faulty trigger switches. This technical overview breaks down the complete assembly architecture, cross-references critical part numbers, and details correct teardown and rebuilding procedures.
Tweco MIG Gun Parts Diagram Component Breakdown
Every industrial Tweco welding torch relies on four primary structural sections: the front-end consumable stack, the conductor tube assembly, the handle and trigger housing, and the rear cable-to-feeder connection block. According to manufacturer specifications, each sub-assembly must maintain strict dimensional alignment to prevent electrical resistance spikes and wire feeding drag.
Recommended Best Deal Products

Front-End Consumables Subassembly
The front end of the torch handles high thermal loads and shielding gas delivery. The primary components shown on the structural schematic include:
- Gas Nozzle: Directs the laminar flow of shielding gas over the weld puddle. Available in slip-on (e.g., 21-50, 22-50) or thread-on (e.g., 23-62) configurations using heavy-wall brass or copper construction.
- Contact Tip: Transfers welding current directly into the solid or flux-cored electrode wire. Common OEM standards include the 11-series (light duty), 14-series (heavy duty), and 14H-series (high-heat copper alloy) engineered for wire diameters from 0.023 in (0.6 mm) to 1/16 in (1.6 mm).
- Gas Diffuser: Threaded onto the conductor tube (models 51, 52, or 54A), holding the contact tip firmly while dispersing shielding gas evenly through radial ports.
- Nozzle Insulator: Prevents electrical shorts between the energized diffuser/tip assembly and the outer gas nozzle body (models 32 or 34A).
Conductor Tube and Cable Connection System
The conductor tube—commonly called the gooseneck—is constructed from armor-jacketed copper tubing available in standard 45°, 60°, or 180° straight bend angles. It channels both the welding current and wire electrode while housing the internal gas tube path. The cable assembly behind the handle features a coaxial copper conductor braid wrapped in a heat-resistant neoprene outer jacket. Internal microswitch control leads run parallel to the main power cable to carry the 24V AC/DC feeder trigger signal.
| Component Reference | Tweco No. 2 Series Part # | Tweco No. 4 / Spray Master Part # | Technical Function |
|---|---|---|---|
| Contact Tip (.035″) | 11-35 / 14-35 | 14-35 / 14H-35 | Current transfer & wire guidance |
| Gas Diffuser | 51 (Thread-on) | 54A (Heavy Duty) | Gas distribution & tip retention |
| Gas Nozzle (1/2″ Bore) | 22-50 | 24A-50 | Shielding gas envelope delivery |
| Conductor Tube (60°) | 62-60 | 64-60 | Current, gas & liner delivery neck |
| Steel Cable Liner (.035-.045″) | 42-3035-15 | 44-3545-15 | Internal low-friction wire conduit |
Interpreting the Tweco MIG Gun Parts Schematic and Layout

Reading a technical schematic for a Tweco torch requires understanding how physical paths overlay electrical and pneumatic lines. On a standard engineering diagram, numerical callouts move from the front gas cup back to the machine pin connector block.
When tracing the system layout, follow three distinct functional paths shown in the schematic:
- The Wire Feed Path: The solid filler wire originates at the wire feeder, enters the rear adapter block via the inner conduit liner guide, passes through the flexible coiled-steel cable liner, traverses the bend of the conductor tube, passes through the center port of the gas diffuser, and exits through the bore of the contact tip.
- The Shielding Gas Path: Gas enters under regulated pressure at the rear termination block fitting. It flows through an internal rubber gas hose running inside the outer cable shell (or directly through the sealed coaxial chamber depending on series year), enters the rear of the gooseneck tube, travels around the outside of the steel liner, and discharges radially through the gas diffuser holes into the nozzle chamber.
- The Primary Electrical Circuit: High-amperage direct current (DCEP/DCEN) travels from the welder’s output terminal through the rear connector block pin, into the heavy copper cabling braid inside the rubber jacket, through the brass hex block at the base of the handle, down the conductor tube, and into the diffuser. Contact with the inner diameter of the contact tip energizes the welding wire.
Tightening Torque Specs: Gas diffusers must be torqued to 10–12 ft-lbs (13.5–16.2 Nm) onto the conductor tube to prevent gas leaks and high electrical resistance. Contact tips require hand-tight installation plus a 1/4-turn (approx. 2–3 ft-lbs) using a dedicated tip wrench. Over-tightening will strip the copper brass threads on the diffuser.
Replacing Components Using the Tweco MIG Gun Parts Diagram

Performing preventive maintenance or replacing worn parts requires a methodical approach to maintain electrical continuity and smooth wire feeding. Follow these step-by-step procedures when tearing down a gun using the exploded schematic as your baseline guide.
Disassembly and Consumable Inspection
Isolate the welding machine from primary input power and close the shielding gas cylinder valve before starting work. Pull off or unscrew the gas nozzle to inspect for spatter accumulation or insulator degradation. Use a specialized MIG tool to unscrew the contact tip counter-clockwise. Inspect the contact tip keyhole wear (bores worn oval cause micro-arcing and erratic feeding). Unscrew the gas diffuser to inspect the rubber O-rings (where applicable) and clear clogged gas ports using a soft wire brush.
Replacing and Trimming the Conduit Liner
Proper installation during a MIG welder liner replacement is the single most critical factor in eliminating wire chatter and feed motor overloading.
- Lay the gun and cable assembly completely straight on a flat floor.
- Unscrew the rear liner retaining nut located on the feeder adapter plug at the machine end.
- Grasp the end of the old liner and pull it completely out from the rear adapter block.
- Unpack the new steel coiled liner and carefully feed it into the gun’s rear block until it seats firmly against the gas diffuser shoulder at the front of the gooseneck.
- Thread the liner retaining nut over the liner and torque it securely into the rear connector block.
- Move to the front of the torch. With the nozzle, contact tip, and diffuser removed, verify that the liner protrudes past the front end of the conductor tube.
- Using high-grade flush cutters, cut the excess liner so it extends exactly 5/8 in (15.9 mm) beyond the end of the bare conductor tube (for standard 51/54A diffusers). Deburr the cut edge using a fine needle file or wire rod to prevent snags.
- Thread the gas diffuser back onto the neck tube until tight, locking the liner securely in place inside the recess of the diffuser.
Cutting the conduit liner too short creates a gap between the end of the liner and the rear of the gas diffuser. Electrode wire will flex and bend into this gap, leading to severe wire bird-nesting, chatter, and complete feeding failure during operation.
Handle and Trigger Microswitch Maintenance
Remove the handle screws and separate the two plastic handle halves. Inspect the microswitch trigger assembly. Verify that the two low-voltage control wire spade connectors are firmly attached to the microswitch terminals. Ensure the steel spring mechanism provides positive snap-action return. Blown or shorted trigger wires usually manifest as a wire feeder that continuously runs or fails to activate when the switch is depressed.
Troubleshooting Failures with Tweco MIG Torch Schematics
When diagnostic issues occur on the shop floor, cross-referencing operational symptoms against diagram failure points shortens downtime. Refer to the diagnostic matrix below for rapid troubleshooting during routine welding gun maintenance.
| Symptom | Diagram Reference Area | Root Cause Analysis | Corrective Action Step |
|---|---|---|---|
| Erratic Wire Feeding / Chatter | Cable Liner & Contact Tip | Liner clogged with metal dust or ovalized contact tip bore. | Blow out liner with compressed air; replace tip (14-series) and check liner stickout. |
| Weld Porosity / Pinholes | Gas Diffuser & Nozzle O-rings | Clogged diffuser ports, loose gas nozzle, or missing rear pin O-rings drawing in air. | Clean diffuser gas holes, inspect nozzle insulator 32/34A, verify shielding gas flow setup. |
| Torch Handle Runs Hot | Conductor Tube Connection Block | Loose locking screw on gooseneck base causing high electrical resistance junction. | Tighten neck locking nut/screw to OEM torque specs; check cable lug crimp. |
| Wire Burns Back to Tip | Contact Tip & Feeder Drive Rolls | Slipping drive rolls or excessive friction inside neck liner curve. | Replace worn contact tip, adjust drive roll tension, ensure minimum cable bend radius (>18 inches). |
| Feeder Does Not Trigger | Handle Switch & Control Pins | Broken control wire in cable assembly or oxidized trigger switch contacts. | Perform continuity test across machine pin plug; replace microswitch or repair spade connectors. |
When running continuous high-amperage spray transfer or metal-cored wire applications, always step up from standard 11-series to heavy-duty 14H series (heavy wall) contact tips and solid brass diffusers (54A series). This increases thermal dissipating mass and extends tip life under high duty cycles.
Tweco MIG Gun Parts Diagram Technical FAQ
How do I determine if my torch uses standard 14-series consumables or Velocity series consumables?
Standard Tweco MIG guns (No. 2, No. 3, No. 4, and Spray Master) utilize traditional threaded gas diffusers (52/54A series) and slip-on or thread-on contact tips (11 or 14 series). The modern Tweco Velocity series uses threadless drop-in contact tips with an integrated gas diffuser profile, secured by a twist-lock retaining cap. Check your conductor tube thread layout on the parts blueprint: standard series feature external threads on the diffuser end, while Velocity necks utilize smooth keyway recesses.
What is the correct procedure for measuring liner stickout on Tweco Spray Master guns?
Insert the new liner fully into the cable from the rear block until it hits the internal stop inside the front gas diffuser. Thread and tighten the rear liner nut at the machine adapter plug first. Next, remove the front diffuser. Mark the liner at the end of the bare conductor tube, extend it outward, and cut it so that exactly 5/8 inch (15.9 mm) extends beyond the neck face. Re-install the diffuser to apply spring pressure against the liner brass collar, securing it in place.
Why is shielding gas leaking from the rear connection block of my Tweco MIG gun?
Gas leakage at the rear block plug usually stems from missing or damaged dual synthetic rubber O-rings seated on the machine pin plug stem. Refer to the rear adapter section of your Tweco parts diagram to locate the two small rubber seal rings (typically part # 82-2030). Replace both O-rings and apply a light coat of silicone lubricant to prevent pinching during insertion into the drive wire feeder block.
Are conductor tubes interchangeable between Tweco No. 2, No. 3, and No. 4 MIG guns?
No, conductor tubes are sized to match the current capacity, barrel outer diameter, and cable connection block dimensions of specific gun series. A Tweco No. 2 gooseneck uses a smaller thread diameter at the handle connection block compared to a heavy-duty No. 4 or Spray Master 450 neck. Always match the exact series number prefix (e.g., 62-series for No. 2, 64-series for No. 4) when ordering replacement conductor tubes from the schematic breakdown.
How do I test for a faulty trigger switch using a digital multimeter?
Disconnect the MIG gun rear connector block plug from the wire feeder. Set your digital multimeter to measure resistance (Ohms Ω) or continuity sound test. Connect the meter probes to the two small control pins located on the rear adapter block plug. With the trigger released, the meter should read infinite resistance (open circuit). Press and hold the gun trigger: the resistance reading should drop below 0.5 Ohms. A reading above 2.0 Ohms indicates pitted switch contacts or broken wire strands inside the cable harness.
Step-by-Step Guide to Understanding the Tweco Mig Gun Parts Diagram
Identify – Locate your specific Tweco series model number on the handle assembly.
Locate – Find the front-end consumable assembly callouts on the diagram layout.
Reference – Check component ordering for the nozzle, contact tip, and gas diffuser.
Connect/Route – Thread consumables securely and route the replacement liner through the conductor tube.
Verify – Measure wire tip protrusion and check seal integrity at the rear connector.
Troubleshoot – Inspect trigger switch wiring continuity if the wire feeder fails to activate.