3 Cylinder Yanmar Injector Pump Diagram: 2026 Guide
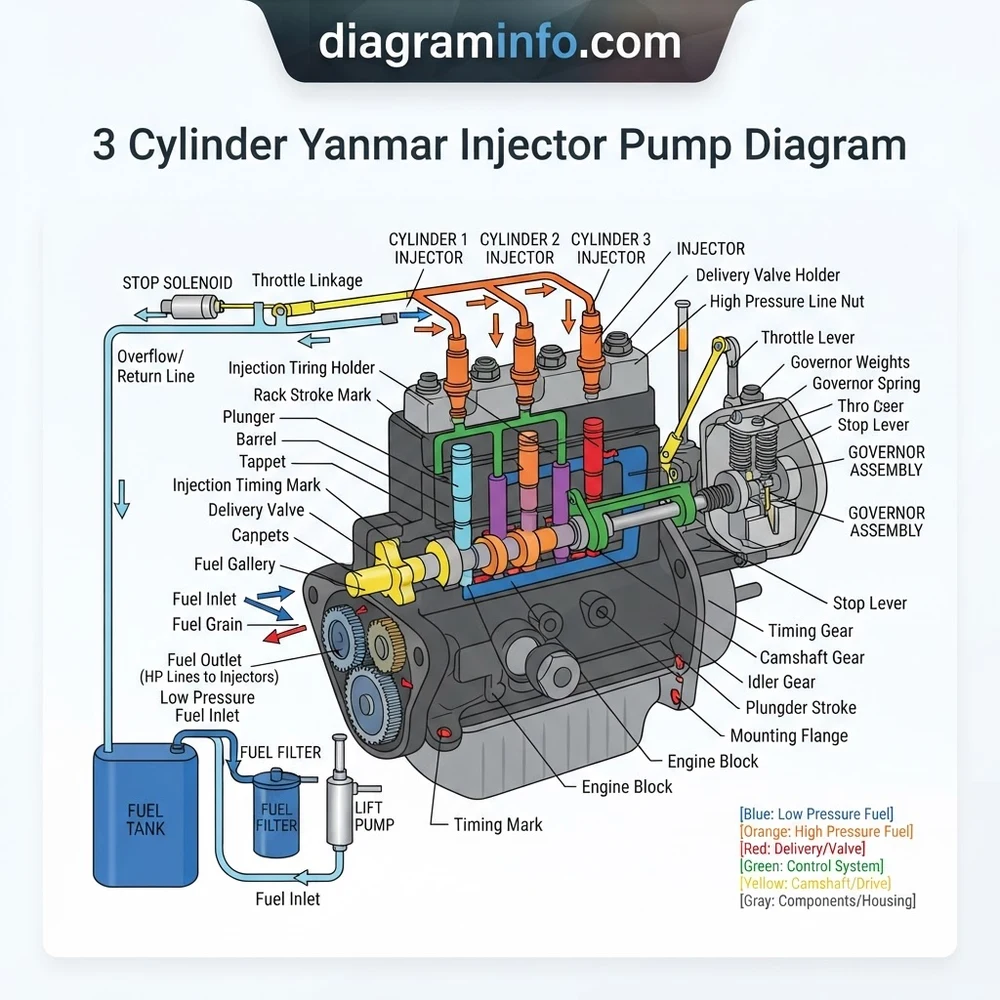
A 3-cylinder Yanmar injector pump diagram details the inline or rotary pump layout, showing fuel supply lines, mechanical governor rack structure, three delivery valves, and banjo bolt torque specs (approx. 18-22 ft-lbs). It illustrates internal plunger alignments and timing mark configurations needed to bleed air and restore fuel pressure.
📌 Key Takeaways
- Injector pump banjo fittings require accurate torque (18-22 ft-lbs) to prevent air intrusion and fuel leaks.
- Delivery valves align sequentially with high-pressure lines feeding cylinders 1, 2, and 3.
- Fuel control rack binding is the leading cause of engine failure to start or engine runaway.
- Engine timing marks on the gear housing must align precisely with the pump flange configuration.
- Internal plunger reassembly requires precision bench testing, whereas seals and line routing are DIY-friendly.
Understanding the mechanical structure and hydraulic flow of a diesel injection system requires a detailed technical reference. A 3 cylinder yanmar injector pump diagram provides field technicians, heavy equipment mechanics, and marine engineers with the schematic roadmap needed to diagnose, service, and rebuild inline and cassette-style fuel injection pumps. Yanmar 3-cylinder diesel engines—commonly found in 3TNV, 3TNE, and 3YM industrial and marine series—rely on high-precision mechanical pump configurations (such as Bosch/Zexel PFR-type or Yanmar MP-series) to generate delivery pressures exceeding 300 bar (4,350 PSI). This guide breaks down the full schematic layout, component interlocks, spill timing procedures, and diagnostic workflows to keep your equipment operating at OEM specs.


3 Cylinder Yanmar Injector Pump Diagram: Mechanical Blueprint Breakdown


The mechanical assembly of a Yanmar 3-cylinder injection pump consists of three distinct hydraulic pumping elements mounted within a shared cast aluminum or iron housing. Each cylinder element is spaced precisely to align with the engine camshaft firing interval (typically 120 crankshaft degrees). Examining the schematic reveals how rotational motion from the engine timing gear train converts into synchronized, metered high-pressure diesel injection.
Plunger-to-barrel clearance: 0.001 mm – 0.002 mm (1–2 microns). Plunger return spring free length: 28.5 mm (service limit: 27.0 mm). Delivery valve cracking pressure: 120–150 bar depending on engine model series (3TNV76 vs 3TNV88).
The core structural parts illustrated on the internal schematic blueprint include:
- Plungers and Barrels: Three ultra-precision machined paired assemblies responsible for building hydraulic pressure. The plunger features a helical control groove (helix) cut into its upper shaft, which governs the effective stroke length and fuel volume delivered per stroke.
- Control Rack and Control Sleeves: A linear gear rack linked to the engine governor. The rack engages pinion gear sleeves surrounding each pump plunger. Slidably moving the rack rotates the plungers, changing the helix position relative to the barrel spill port to regulate fuel volume from idle to full load.
- Delivery Valve Assemblies: Located directly above each barrel outlet, these spring-loaded non-return valves trap residual pressure in the high-pressure steel injection lines (maintaining 10–20 bar baseline pressure) to prevent line cavitation and secondary fuel injection.
- Tappet Assemblies and Roller Bearings: Positioned at the base of each plunger, tappets ride directly on the fuel camshaft lobes. Roller tappets absorb side thrust forces, converting cam rotation into pure vertical linear displacement.
- Fuel Stop Solenoid: An integrated 12-volt DC actuator configured as either Energize-To-Run (ETR) or Energize-To-Stop (ETS). The solenoid plunger acts directly on the governor link or rack arm to cut off fuel supply instantly upon key switch deactivation.
| Diagram Callout | Component Name | OEM Function / Specification | Torque Specs (Nm) |
|---|---|---|---|
| 1 | Delivery Valve Holder | Secures valve assembly to pump housing | 39 – 44 Nm (29–32 ft-lbs) |
| 2 | High-Pressure Line Fitting | Attaches hard line to delivery holder | 25 – 29 Nm (18–21 ft-lbs) |
| 3 | Pump Mounting Flange Bolts | Secures pump body to engine gear case | 22 – 25 Nm (16–18 ft-lbs) |
| 4 | Fuel Stop Solenoid Body | Controls rack shutdown mechanism (12V DC) | 15 – 20 Nm (11–15 ft-lbs) |
| 5 | Bleed Screw Assembly | Vents air from low-pressure gallery | 8 – 10 Nm (6–7 ft-lbs) |
How to Interpret the Yanmar 3-Cylinder Fuel System Configuration


Reading a schematic or layout diagram correctly is crucial when performing timing adjustments, bench testing, or chasing intermittent fuel starvation issues. The layout details two distinct pressure zones within the engine bay: the low-pressure supply loop and the high-pressure injection circuit.
For step-by-step air elimination procedures after replacing pump gaskets or lines, consult our comprehensive Yanmar fuel system bleeding guide.
1. Tracing the Low-Pressure Supply Pathway
In the diagram, low-pressure diesel flows from the fuel tank through a primary water separator, entering the mechanical lift pump driven by the engine camshaft. The lift pump pressurizes fuel to approximately 0.2 to 0.4 bar (3 to 6 PSI) and forces it through a 5-micron secondary filter into the injection pump internal gallery. Excess fuel inside the gallery passes through an overflow valve equipped with a calibrated orifice, which bleeds air back to the fuel tank while maintaining static gallery pressure.
2. High-Pressure Metering and Firing Sequence


The schematic indicates high-pressure delivery channels exiting vertically from the top of the pump housing. For standard Yanmar 3-cylinder engines (such as the 3TNV88), the firing order is conventionally 1 – 3 – 2 or 1 – 2 – 3 relative to flywheel position. As the internal or external fuel camshaft rotates, each lobe forces its respective tappet and plunger upward. Once the plunger closes the barrel inlet port, fuel compression begins immediately, pushing open the spring-loaded delivery valve and sending a shockwave of pressurized fuel to the nozzle injector at 190–220 bar opening pressure.
3. Spill Timing and Shim Thickness Calculations
Yanmar cassette-style pumps use precision ground steel shims under the pump mounting flange to set static injection timing (expressed in degrees Before Top Dead Center, or °BTDC). Interpreting the diagram’s timing reference marks requires understanding the inverse relationship between shim thickness and injection timing:


- Adding Shim Thickness (Thicker Shim): Moves the pump body higher, relative to the camshaft. The camshaft lobe contacts the tappet later in its rotation, which retards injection timing.
- Subtracting Shim Thickness (Thinner Shim): Lowers the pump body closer to the camshaft. The cam lobe contacts the tappet earlier, which advances injection timing.
- Rule of Thumb Spec: A change of 0.1 mm in shim thickness alters static injection timing by approximately 1.0 degree of crankshaft rotation.
3 Cylinder Yanmar Injector Pump Diagram Diagnostics and Fixes


When diagnosing engine misfires, hard starting, or black smoke emissions, comparing observed physical conditions against the schematic layout allows you to isolate hydraulic failure points quickly.
High-pressure diesel spray under 300+ bar can penetrate human skin tissue, causing severe necrosis. Always wear safety glasses and pressure-rated gloves. Before starting an engine after injection pump reinstall, ensure the intake air shutoff valve or a thick rubber block is available to starve the air intake in case of runaway caused by a stuck control rack.
Symptom Isolation and Root Cause Analysis


When working on industrial machinery, consult the factory 3TNV88 engine service manual or related OEM documentation alongside your schematic. Below is a structured diagnostic reference table matching physical symptoms to schematic components:
| Engine Symptom | Diagram Component Involved | Root Cause Mechanism | Corrective Field Action |
|---|---|---|---|
| Engine cranks, no start (No fuel at lines) | Stop Solenoid / Internal Rack | Solenoid coil burned out or rack stuck in zero-fuel position | Test coil resistance (1.5–2.5 Ω). Verify 12V supply signal. Inspect rack movement. |
| Misfire on single cylinder, rough idle | Delivery Valve / Plunger Barrel #2 | Broken delivery valve spring or seized plunger due to water contamination | Perform line disconnect test. Inspect delivery spring. Clean or replace pumping element. |
| Excessive black smoke under engine load | Pump Base Shim / Helix Wear | Advanced injection timing (too thin shim) or worn plunger helix delivering excess fuel | Re-check spill timing using spill tube tool. Increase timing shim thickness as needed. |
| Engine hunting or surging RPM at idle | Mechanical Governor Assembly | Worn flyweight thrust washer or binding rack linkage connection | Perform a Bosch/Zexel mechanical governor adjustment and inspect linkage pins for binding. |
Procedure: Checking Spill Timing via the Schematic Reference
- Disconnect the high-pressure fuel line from cylinder #1 delivery valve holder.
- Remove the internal delivery valve, spring, and valve seat, then reinstall the holder body with a clear plastic spill tube attached.
- Rotate the engine flywheel manually in the normal direction of rotation (counterclockwise from flywheel end) while operating the manual fuel primer pump.
- Watch the fuel stream exiting the spill tube. The exact moment fuel stops flowing from the tube corresponds to the spill cutoff point (port closure).
- Check the timing mark stamped on the flywheel against the timing pointer on the flywheel housing. If the degrees registered do not match OEM spec (e.g., 14° BTDC ± 1°), adjust the shim pack beneath the injection pump body accordingly.
3 Cylinder Yanmar Injector Pump Diagram FAQ and Technical Specs
What is the standard resistance reading for a Yanmar 3-cylinder fuel stop solenoid?


On standard 12-volt DC ETR (Energize-To-Run) solenoids used in Yanmar 3-cylinder engines, the pull-in coil resistance measures between 0.2 and 0.4 ohms (drawing approximately 30–40 amps for a split second), while the hold-in coil resistance measures between 1.2 and 2.5 ohms (drawing approximately 1.0–1.5 amps continuous). If resistance reads infinite or zero, the solenoid coil has failed internally and must be replaced.


How do I identify whether my Yanmar injection pump uses internal or external timing marks?
Refer to the engine front timing case on the diagram layout. Direct-injection 3TNV and 3TNE series engines generally feature an engraved timing line on the pump flange that aligns with a mating mark stamped into the engine gear case cover. Older pre-combustion chamber engines (like the 3D84 or 3YM series) rely on flywheel timing marks combined with static spill timing via shim height measurement rather than gear case scribes.
Why is fuel weeping out of the bleed screw threads on the injection pump body?
The bleed screw assembly shown on the low-pressure gallery diagram utilizes a soft copper or aluminum crush washer to seal against the cast housing. Torque specs for this fitting are low (8–10 Nm). Reusing a hardened or deformed crush washer, or over-tightening the screw, will strip the fine aluminum threads on the pump body. Always install a new copper washer and torque to factory specifications.
What causes a single delivery valve to stick open on a 3-cylinder Yanmar pump?
A stuck delivery valve is almost universally caused by ultra-fine particle contamination or water intrusion passing through damaged fuel filtration elements. Water causes localized corrosion pitting on the micro-finished seating surface of the valve plunger, binding it inside its bore. When stuck open, high-pressure line pulsations collapse, resulting in a severe cylinder misfire and white smoke in the exhaust.
Can I swap an injection pump from a Yanmar 3TNV84 onto a 3TNV88 engine?
While the physical mounting flange footprint and 3-cylinder layout appear identical on external schematic blueprints, the internal plunger diameters and cam lobe lift profiles differ. The 3TNV88 features a larger cylinder bore and requires a larger fuel displacement per stroke (plunger diameter is typically 0.5 mm larger). Installing a 3TNV84 pump on a 3TNV88 engine will lead to lean fuel delivery, severe power loss, and elevated exhaust gas temperatures (EGT) under load.
Step-by-Step Guide to Understanding the 3 Cylinder Yanmar Injector Pump Diagram
Identify – Examine the 3 cylinder yanmar injector pump diagram to locate primary components, control rack, and delivery ports.
Locate – Find the fuel inlet line, manual air bleed screw, and high-pressure line fittings on the pump body.
Reference – Match diagram layout callouts to physical timing marks on the pump flange and engine front housing.
Connect/Route – Route fuel lines from pump delivery valves to each injector following numbered cylinder sequence.
Verify – Check banjo bolt torque specifications and purge trapped air through the bleed screw before cranking.
Troubleshoot – Consult the diagram flow if uneven idle, fuel starvation, or line leaks persist during startup.