Yamaha Flute Parts of a Flute Diagram: 2026 Component Breakdown
A standard C concert flute structure consists of three main sections: headjoint, body, and footjoint. The headjoint contains the crown, cork assembly, lip plate, and embouchure hole. The body houses the main key mechanism layout, tone holes, and steel rods. The footjoint configures the low C/C# or B keys.
📌 Key Takeaways
- Headjoint cork stopper depth must sit exactly 17.3 mm from the center of the embouchure hole.
- Key alignment relies on steel rods, pivot screws, and delicate needle springs rated at standard tension.
- Pad seating tolerances require under 0.01 mm clearance to prevent air leaks across tone holes.
- The most common mechanical failure point is displaced needle springs or dried headjoint cork seals.
- Basic cleaning and rod oiling are DIY friendly, but key repadding and tone hole leveling require technician tools.
In high-precision machining, tooling engineering, and industrial equipment manufacturing, interpreting schematic blueprints of cutting geometry is essential for optimizing metal removal rates, tool life, and surface finish quality. Precision tools such as solid carbide end mills, twist drills, reamers, and fluted hydraulic valve spools rely on meticulously engineered channel geometry to evacuate swarf, direct coolant flow, and maintain structural rigidity under extreme shear stresses. Understanding every engineering detail represented in a standardized blueprint enables CNC programmers, toolmakers, and maintenance technicians to select the correct tooling, verify manufacturing tolerances, and diagnose premature failure modes. This technical guide breaks down the full architectural layout, cross-sectional specifications, reading protocols, and troubleshooting workflows required to analyze complex tool schematics effectively.


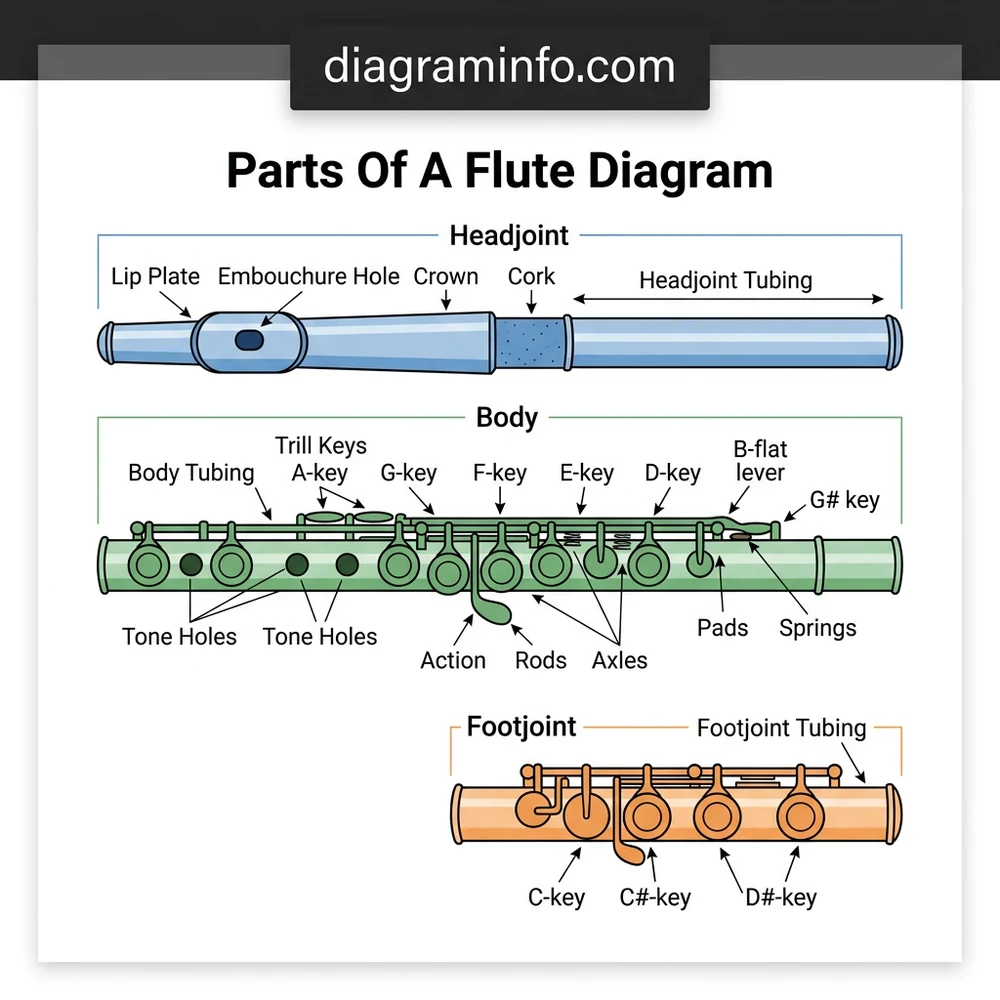
Parts Of A Flute Diagram: Structural Component Breakdown


A comprehensive tooling blueprint details both the external geometry and internal core structure of the channel layout. Every functional element in the engineering schematic is designed to balance chip evacuation volume against overall tool column stiffness according to rigid DIN and ISO standards.
Cutting Edge, Primary Land, and Margin Configuration
The cutting edge represents the primary interface where material shearing occurs. Situated immediately behind the cutting edge is the primary land, which provides structural backing to prevent edge chipping under heavy chip loads. The margin—a narrow, raised cylindrical land section running along the outer diameter of the flute helix—guides the tool inside the hole or cut, controlling radial runout and maintaining hole size tolerances. Behind the margin, the secondary relief angle drops away to clear the workpiece material, reducing friction and localized heat generation during high-speed engagement.
Flute Valley, Web Thickness, and Core Geometry


The flute valley (or gullet) is the concave channel ground into the body of the tool to facilitate smooth chip formation and continuous swarf ejection. The deepest point of the valley defines the web thickness (or core diameter). According to OEM manufacturing specifications, the web core constitutes between 50% and 80% of the total cutting diameter, depending on whether the tool is optimized for deep-hole drilling or heavy roughing. Modern tooling designs incorporate a tapered web core, where the web thickness increases gradually from the tool tip toward the shank at a rate of 0.015 mm to 0.030 mm per 10 mm of flute length to maximum axial rigidity against bending forces.
Helix Angle, Rake Profile, and Relief Layout
The helix angle is formed by the intersection of the helical cutting edge and the longitudinal centerline of the tool body. Standard helix angles range from 30° for general-purpose machining up to 45° or 50° for soft, ductile materials like aluminum alloys. The radial rake angle—measured from a radial line extending from the center of the tool to the cutting edge—determines the sharpness and aggressiveness of the cut. Positive radial rake angles reduce cutting forces and power draw, while neutral or negative rake angles are specified for hardened steels and high-temp superalloys to reinforce the cutting wedge.
| Blueprint Feature | Standard Engineering Range | Primary Mechanical Function | Failure Mode if Out of Spec |
|---|---|---|---|
| Web Thickness Ratio | 55% – 75% of tool diameter | Provides core rigidity against torsional shear | Core snap under high feed loads (<55%) or packing (>75%) |
| Radial Rake Angle | -5° to +18° | Controls chip shearing force and edge sharpness | Edge chipping (too positive) or spindle overload (too negative) |
| Helix Angle Variation | 30° / 35° / 38° (Variable pitch) | Disrupts harmonic chatter during high-speed milling | Severe harmonic resonance and wall chatter marks |
| Margin Width | 0.25 mm – 0.80 mm | Stabilizes tool cylindrical alignment in cut | Galling, friction heat, or hole oversizing/tapering |
| Primary Radial Relief | 6° to 12° | Prevents heel rubbing behind cutting edge | Work hardening of workpiece, high thermal buildup |
How to Read a Parts Of A Flute Diagram Blueprint


Interpreting an industrial schematic requires a systematic approach to reading cross-sectional views, longitudinal cutting planes, geometric dimensioning and tolerancing (GD&T) callouts, and angular reference baselines. Follow this step-by-step technical protocol when reviewing tool layout drawings prior to setup or quality assurance inspection.


Step 1: Orient Axial and Radial Projection Views


Begin by analyzing the primary longitudinal profile view to establish total tool length (OAL), usable flute length (LU), and shank diameter (D2). Locate the cross-sectional cutting plane indicators (typically labeled Section A-A or Section B-B). Cross-sectional projections are drawn perpendicular to the axis of the cutter and reveal the internal web core profile, flute depth, and radial rake orientations.
Step 2: Calculate Web Taper and Core Rigidity Specifications
Examine the core measurement callouts at both the face of the tool and the back of the flute length. Calculate the web taper ratio to ensure compatibility with your machining operation. For deep-cavity milling or long-overhang drilling, perform an end mill cutter geometry analysis to confirm that the moment of inertia provided by the web thickness profile is sufficient to withstand anticipated deflection limits under lateral radial loads.
Step 3: Measure Angular Dimensions and Land Width Tolerances


Identify the helix angle along the outer diameter profile. On variable-helix blueprints, note the differential spacing between individual flute margins (e.g., 88°–92° asymmetric index spacing). Verify the primary land width and radial relief angle on the sectional view. Use micro-calibrated optical comparators or tool presetters to confirm that manufactured tolerances match blueprint limits within ±0.002 mm (2 microns).


According to ISO 13399 standards for digital cutting tool data representation, radial runout across all flute margins must not exceed 0.003 mm total indicator reading (TIR) relative to the shank reference axis. Standard web concentricity tolerances on premium micro-grain tungsten carbide substrates must be held to within h6 shank specifications to guarantee dynamic balance at speeds exceeding 15,000 RPM.
Step 4: Inspect Surface Finish and Coating Layer Callouts
Review the blueprint notes section for surface roughness ratings along the flute valley floor. Flute surfaces require micro-polishing to achieve a surface finish of Ra 0.1 µm to Ra 0.2 µm (4 to 8 micro-inches). Verify Physical Vapor Deposition (PVD) or Chemical Vapor Deposition (CVD) coating layer specifications. Advanced multi-layer coatings such as Titanium Aluminum Nitride (TiAlN) or Aluminum Titanium Silicon Nitride (AlTiSiN) are typically applied at a uniform thickness of 2.0 to 4.0 microns across the cutting lip and land, while maintaining a smooth, un-coated or ultra-slick friction coefficient within the flute gullet to optimize swarf ejection.
When reviewing blueprint specifications for heavy-duty metal removal, cross-reference tool geometry with the underlying carbide substrate metallurgy. Substrates containing 10% cobalt binder offer superior transverse rupture strength (TRS) for tools with aggressive positive radial rake angles, whereas 6% cobalt sub-micron grades are specified for high-rigidity designs operating under high thermal loads.
Troubleshooting Flute Geometry Failure Modes on the Shop Floor



When cutting tools, reamers, or fluted hydraulic components suffer premature failure, analyzing wear patterns against the original layout schematic provides critical diagnostic data. The following technical troubleshooting matrix maps physical damage back to geometric design flaws or operational misalignments.
Addressing Flute Clogging and Chip Evacuation Failures
If chips become packed tightly inside the flute valley during operation, immediate thermal friction spiking occurs, leading to cataclysmic tool breakage. Clogging indicates that chip volume exceeds the available cross-sectional gullet area shown in the blueprint layout. To resolve this, increase coolant supply pressure (minimum 70 bar / 1000 PSI for through-tool systems), decrease feed per tooth ($f_z$), or select a tool layout featuring a smaller web core ratio and a higher helix angle to accelerate axial chip transport.
Mitigating Chipping along the Flute Margin and Cutting Edge
Micro-chipping along the primary margin or cutting edge typically stems from excessive radial runout, excessive primary relief clearance, or structural chatter. Check total system runout at the spindle interface; total runout exceeding 0.005 mm causes uneven chip loading per flute, overloading one margin section while under-utilizing others. Execute a thorough CNC tool holder runout calibration procedure on high-precision hydraulic expansion chucks or shrink-fit holders to eliminate runout variance.
During tool re-sharpening, altering the factory primary radial relief angle specified on the parts of a flute diagram by more than ±1.5° severely compromises edge strength. Decreasing the relief angle leads to rear land rubbing, localized frictional heat exceeding 800°C, and rapid thermal cracking. Increasing the relief angle weakens the wedge support, causing edge collapse under impact loads.
Managing Thermal Micro-Cracking and Coating Delamination
Vertical hairline cracks propagating perpendicular to the cutting edge (thermal fatigue cracks) indicate extreme thermal cycling during interrupted cuts. Check whether the blueprint specifies a wet or dry cutting geometry. For high-speed dry machining of hardened steels (50–65 HRC), ensure the tool utilizes an ultra-fine grain carbide matrix combined with a high-heat-resistant nano-composite PVD coating, and replace flood coolant with air-blast purge to prevent thermal shock.
Technical FAQ: Parts Of A Flute Diagram and Tooling Layouts
How does web taper impact structural rigidity and chip space in tool schematics?
Web taper increases the core diameter of the tool from the tip toward the shank base at a controlled linear slope (typically 1.5% to 3.0% back taper). Near the point of the tool, the smaller core diameter maximizes flute valley volume for chip generation and immediate evacuation. Near the shank, the enlarged core diameter increases the polar moment of inertia, significantly raising bending stiffness and resistance to torsional strain during deep axial milling or drilling operations.


What is the primary difference between land width and margin width on a flute blueprint?
The primary land width refers to the ground surface directly behind the cutting edge that incorporates the primary relief angle; it supports the cutting wedge during material shearing. The margin width refers specifically to the narrow, un-relieved narrow band on the absolute outer diameter of the flute that physically contacts the bore wall or cut surface, providing guide stability, controlling tool alignment, and burnishing the wall surface to achieve target micro-inch surface finishes.
Why do modern high-performance tooling blueprints specify variable helix and asymmetric pitch designs?
Standard uniform-helix tools generate constant mechanical impact frequencies during multi-flute rotational engagement, inducing severe harmonic vibration (chatter) at specific spindle speeds. By varying the helix angle across individual flutes (e.g., alternating between 35° and 38°) or altering the radial indexing angle between margins (asymmetric pitch), the impact frequency pattern is randomized. This breaks phase resonance, dramatically suppressing chatter and allowing higher depths of cut (axial $a_p$) at elevated feed rates.
What tolerance standards govern radial runout across flute margins on solid carbide tooling?
Precision solid carbide tooling is manufactured in accordance with DIN 6537 and ISO 13399 standards. Total radial runout measured from the shank axis across all flute margins must not exceed 0.003 mm (3 microns) for standard tool classes, and 0.0015 mm (1.5 microns) for micro-machining tools below 3.0 mm diameter. Exceeding these runout tolerances leads to disproportionate flute loading, accelerated single-edge wear, poor surface finishes, and premature catastrophic core failure.
How does flute surface roughness affect chip evacuation efficiency?
The surface finish inside the flute gullet dictates the coefficient of friction encountered by continuous metal chips during shearing. A rough ground surface (Ra > 0.4 µm) increases frictional resistance, slowing chip velocity and encouraging built-up edge (BUE) formation, particularly in sticky non-ferrous materials such as 6061 aluminum or Ti-6Al-4V titanium. Polishing the flute valley floor to Ra 0.1 µm or better reduces sliding friction, allowing uninterrupted chip flow, lower operating temperatures, and higher volumetric material removal rates (MRR).
Step-by-Step Guide to Understanding the Parts Of A Flute Diagram
Identify – Locate the headjoint, body, and footjoint sections using the structural system diagram.
Locate – Check headjoint cork position by inserting a cleaning rod to verify the notch centers in the embouchure hole.
Reference – Inspect key layout along the body tube, referencing needle spring connection points on every post.
Align – Join headjoint to body, aligning embouchure hole center with the main line of body keys.
Verify – Insert a leak light into the body structure to confirm uniform 360-degree pad seating on tone holes.
Troubleshoot – If keys fail to rebound, inspect the diagram’s spring configuration and re-seat dislodged steel springs using a spring hook.