Inogen One G5 Parts Diagram: 2026 Repair Guide
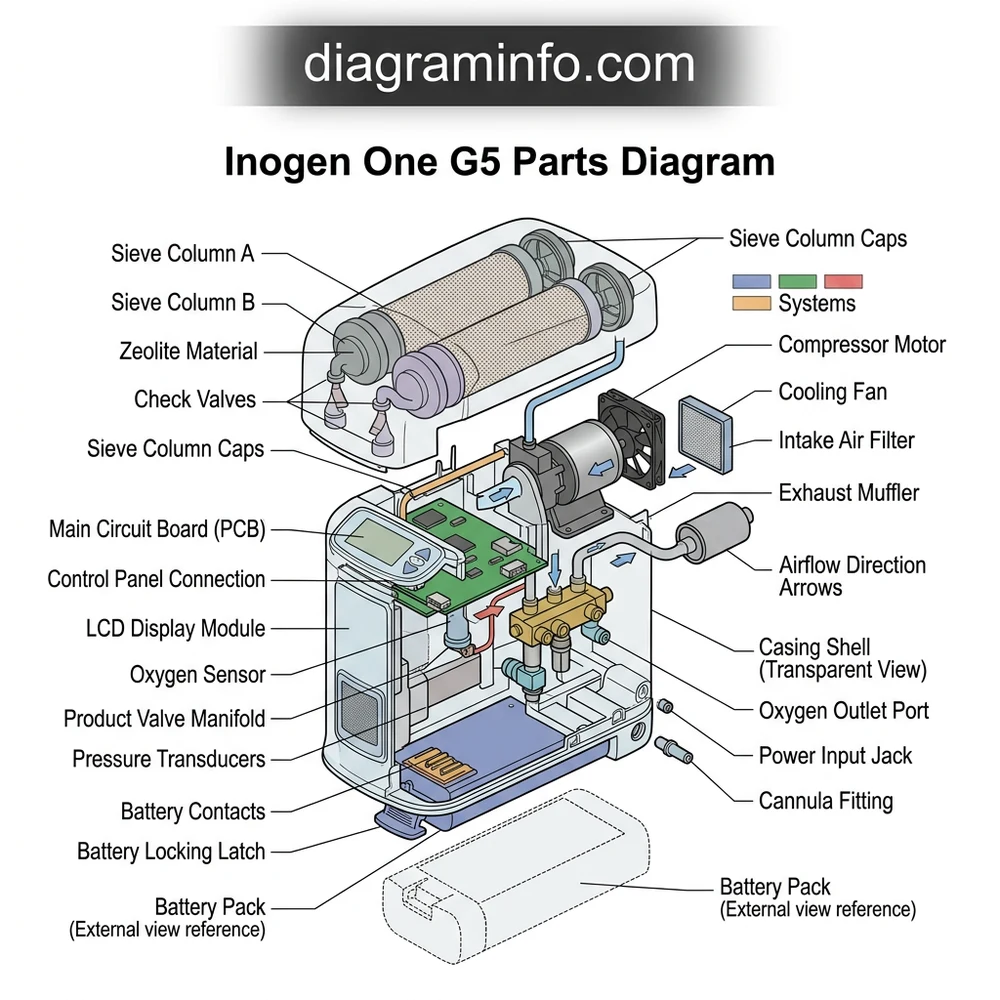
The Inogen One G5 parts diagram maps the internal layout, including the dual sieve column beds (RP-502), micro-compressor assembly, DC input connector, main control PCB, particle inlet filters, and oxygen outlet port. It outlines internal tubing routing, wiring harnesses, and component mounting points critical for servicing sieve columns or replacing damaged exterior housing.
📌 Key Takeaways
- Sieve columns (RP-502) require routine replacement when column life alerts appear, typically every 12 to 18 months.
- Primary electrical input runs on 12-15V DC via the external power jack connected directly to the power management board.
- Critical internal flow connections use 1/8-inch silicone pressure tubing secured with micro spring clamps to prevent leaks.
- The micro-compressor is the main internal wear component, highly sensitive to dust ingress if particle filters are neglected.
- Filter and sieve bed replacements are user-serviceable DIY tasks, whereas compressor or internal circuit repairs require certified technicians.
The Inogen One G5 portable oxygen concentrator relies on an intricate balance of pneumatic flow, high-pressure switching, and microprocessor-controlled oxygen delivery. Servicing and maintaining this compact medical-grade unit requires a deep understanding of its internal mechanical and electrical structure. Utilizing a precise Inogen One G5 parts diagram allows service engineers, biomedical technicians, and experienced repair specialists to isolate faulty pneumatic lines, replace high-wear components like sieve columns, and trace low-voltage control signals across the system PCB. This technical teardown details the internal layout, schematic pathways, component specs, and diagnostic procedures required for complete equipment maintenance.


Inogen One G5 Parts Diagram: Component Breakdown and Internal System Layout


The internal structural architecture of the Inogen One G5 is engineered to maximize liter-per-minute (LPM) pulse-dose output while maintaining a lightweight form factor. The exploded view of the unit reveals six primary modular subsystems integrated into a high-impact polycarbonate chassis. Understanding the exact spatial orientation and interconnection of these parts is critical prior to performing system disassemblies or component swaps.
Always replace the sieve column seals (O-rings) whenever servicing the manifold interface. Degradation of the Viton rubber fluoroelastomer seals causes micro-leaks, leading to a rapid reduction in delivery pressure and triggering low O2 purity alerts.
1. Micro-Compressor Assembly (OEM P/N: RP-500)
The compressor serves as the heart of the pneumatic system. It features a dual-cylinder, oil-free wobbling piston mechanism powered by a 24V DC brushless motor. Operating at variable RPMs dependent on the oxygen flow setting (1 through 6), the compressor draws ambient air through an external particulate screen and intake silencer, forcing pressurized air into the valve manifold at dynamic pressures ranging between 18.5 PSI and 28.0 PSI.
2. Sieve Bed Columns (OEM P/N: RP-502)

Positioned vertically adjacent to the compressor housing, the twin sieve columns contain a densely packed bed of Lithium-X (LiX) molecular sieve zeolite. Using Pressure Swing Adsorption (PSA) technology, these columns alternate cycles: one column adsorb nitrogen from pressurized ambient air to produce up to 96% pure oxygen, while the opposite column vents nitrogen gas out through the exhaust muffler.
3. Solenoid Valve Manifold Block
Mounted directly above the sieve columns, the aluminum manifold configuration contains five high-frequency miniature solenoid valves. Four valves handle the alternating feed and purge cycles between Sieve Columns A and B, while the fifth valve functions as the equalizer valve to normalize column pressure before cross-over switching.
4. Main Logic Control Board (PCB) & Ultrasonic Sensor


The main circuit board mounts parallel to the front casing. It houses the primary ARM Cortex control processor, low-pressure piezoresistive differential transducers, compressor PWM motor drivers, and an ultrasonic oxygen concentration sensor module. The sensor continuously calculates output purity by measuring the speed of sound through the purified gas stream.


| Component Name | OEM Part Reference | Operating Specification | Service Life / Maintenance |
|---|---|---|---|
| Dual Piston Compressor | RP-500 | 24V DC / 18.5–28.0 PSI output | Inspect every 5,000 hours |
| Sieve Bed Pair Assembly | RP-502 | LiX Zeolite / Synthetic Matrix | 12 to 24 months (User replaceable) |
| Solenoid Manifold Block | RP-505 | 12V DC Switching / 5-Valve Array | Replace on physical valve latch failure |
| Particle Intake Filter Set | RP-501 | Washable Synthetic Mesh | Clean weekly / Replace yearly |
| Ultrasonic Flow/O2 Sensor | RP-509 | 82.0% – 96.0% O2 Detection Range | Board-integrated calibration |
How to Read the Inogen One G5 Schematic Blueprint and Flow Configuration


Interpreting an Inogen One G5 schematic blueprint requires analyzing two distinct functional layers: the pneumatic fluid circuit and the electrical wiring harness network. When troubleshooting performance drops, technicians must cross-reference pressure transducer outputs on the electrical circuit map with physical flow paths shown on the pneumatic schematic. For further details on general concentrator designs, consult our portable oxygen concentrator repair guide.
System Oxygen Concentration: 90% +6% / -3% across all pulse settings (1 to 6). Nominal dynamic system balance pressure: 22.5 PSI at sea level. Max power draw: 120W during peak battery charging and setting 6 operation.
Tracing the Pneumatic Flow Circuit
Follow these exact sequential stages on the pneumatic overview layout during complete trace analysis:
- Stage 1 (Air Intake): Ambient air passes through the intake filter screen into the noise-damping plenum, filtering out particles larger than 5 microns.
- Stage 2 (Compression): The twin-cylinder compressor compresses air to ~22 PSI, feeding it through a stainless steel heat exchanger loop to reduce air temperature before entering the valve block.
- Stage 3 (PSA Cycle Shift): Solenoid Valve 1 opens, routing pressurized air into Sieve Column A. Nitrogen is adsorbed by the zeolite, and pure oxygen flows through a non-return check valve into the product storage manifold. Simultaneously, Solenoid Valve 2 vents column B to atmosphere via the exhaust silencer.
- Stage 4 (Pulse Delivery): Highly concentrated oxygen stored in the product tank passes through a proportional pulse delivery solenoid valve. The valve pulses upon detecting negative inhalation pressure via the differential pressure sensor connected to the patient cannula port.
Reading the Main Board Wiring Diagram and Pinouts


Electrical connectivity within the G5 configuration is established through high-density ribbon cables and locking Molex-style connectors. Refer to the electrical blueprint pinout specs below when probing points with a digital multimeter:
| Connector Header | Wire Harness Pin & Color | Signal Type / Function | Expected Nominal Voltage |
|---|---|---|---|
| J1 – Motor Power | Pin 1 (Red) / Pin 2 (Black) | Compressor DC Power Supply | 19.0V DC – 24.0V DC |
| J1 – Motor Control | Pin 3 (Yellow) | PWM Speed Control Signal | 0.5V – 4.8V PWM |
| J2 – Solenoids | Pins 1–5 (Blue/White) | Valve Coil Driver Triggers | 12.0V DC Pulsed |
| J3 – Sensor Bus | Pin 1 (Green) / Pin 2 (Bare) | Pressure Transducer Analog Signal | 0.5V DC (0 PSI) to 4.5V DC (30 PSI) |
Troubleshooting Common Failures via the Inogen One G5 Parts Diagram


Diagnosing operational faults on the G5 requires combining software diagnostic alarm codes with hardware checks on components identified in the schematic diagram. Before tearing down the valve block or replacing expensive control boards, follow systematic diagnostic tree workflows. Technicians working on motor sub-assemblies should also review our brushless compressor rebuild guide for specialized mechanical repair procedures.


Depressurize the pneumatic system entirely before disconnecting any tubing from the sieve beds or compressor outlet. Oxygen-rich high-pressure air bursts can cause eye injuries or sudden ignition if exposed to open flames or grease contaminants.
1. Oxygen Purity Below Threshold (Alarm Code: Low O2 / Error 002)
When the ultrasonic sensor reads an oxygen output below 87%, the main board triggers a low purity notification. Use the diagram to trace the following potential fault points:
- Exhausted Zeolite Columns: Check the operating hour count. If sieve beds exceed their service lifecycle or have been exposed to high humidity, zeolite beads degrade, losing nitrogen adsorption capacity. Replace the sieve column pair (RP-502). For deeply technical information on molecular structure, read our zeolite column material specifications.
- Solenoid Valve Leakage: A stuck equalizer valve allows compressed air to bypass Column A and Column B simultaneously. Verify valve coil resistance across J2 terminals using a multimeter. Normal valve coil resistance must read between 38 Ohms and 44 Ohms.
- Compressor Pressure Drop: Inspect wear on the PTFE cup seals inside the twin-piston compressor housing. If output pressure measures below 18.0 PSI, replace the cup seal ring assembly.
2. Breath Detection Failure / No Pulse Delivery
If the device fails to deliver a pulse of oxygen during inhalation, the issue stems from the piezoresistive differential pressure sensing line:
- Inspect the small-diameter clear silicone sensing tube extending from the brass cannula barb down to the differential pressure port on the main board layout.
- Check for condensation build-up, kinks, or tears in the silicone line that prevent the pressure differential transducer from registering the negative pressure dip (-0.12 cm H2O threshold) caused by patient inhalation.
| Fault Symptom | Probable Cause Component | Diagram Reference Test Point | Corrective Action Step |
|---|---|---|---|
| Error 001 (Thermal Shutoff) | Compressor Thermal Switch / Fan Failure | J4 Fan Header / Temp Sensor | Clean cooling ducts; replace 5V DC micro-fan |
| O2 Purity Drops <87% | Sieve Beds / Manifold Leakage | Sieve Column Base O-Rings | Swap Sieve Columns; re-test purity after 10 min run time |
| Compressor Motor Stalls | Worn Brushless Motor Bearings | J1 Pins 1–2 Wire Terminal | Check current draw (>4.5A indicates mechanical drag); rebuild compressor |
| Continuous Hissing Sound | Ruptured Exhaust Valve Diaphragm | Exhaust Valve Manifold Port | Re-seat or replace solenoid valve block assembly |
Inogen One G5 System Overview and Maintenance FAQ
What are the primary structural differences shown in the G5 diagram compared to the older G3 or G4 configurations?
The Inogen One G5 blueprint incorporates a higher-capacity dual-piston compressor design and larger surface area sieve columns compared to the G4, allowing for 6 pulse settings instead of 4. Furthermore, the G5 features quick-release sieve column retention latches directly on the lower outer housing, enabling users to swap columns without taking apart the main structural frame of the device.
How do I test the ultrasonic oxygen sensor board module on the G5 schematic?
The ultrasonic oxygen sensor is integrated into the primary flow manifold. Connect a calibrated digital multimeter to the signal output pins on header J3. At room air (21% O2), the sensor outputs a baseline voltage near 1.1V DC. When delivering 93% pure oxygen, the steady-state signal rises to approximately 4.1V DC. If signal voltage remains static at zero or exceeds 5.0V DC, the sensor circuit or controller IC requires factory re-calibration or replacement.
What torque specifications apply to the internal chassis and compressor mounting fasteners?
When reassembling the internal structural framework of the G5, torque all main housing chassis screws (Torx T10) to 4.5 in-lbs (0.51 Nm). The compressor mounting bracket dampers must be torqued precisely to 3.8 in-lbs (0.43 Nm) to prevent excessive vibration transfer through the outer enclosure, which can cause premature board component cracking and elevated operational noise levels.
Can individual solenoid valves on the Inogen One G5 manifold be replaced independently?
While the OEM parts manual lists the solenoid manifold block as a unified assembly (P/N: RP-505), individual 12V DC coil caps can be unbolted using precision micro-fasteners. However, bench servicing individual sub-valves requires micro-lap polishing of the aluminum valve seat and replacement of internal micro-springs. For field repairs, swapping the complete integrated manifold block is recommended to maintain certified flow specifications.


How often should internal tubing and pneumatic check valves be replaced according to OEM maintenance blueprints?
Pneumatic silicone delivery lines and synthetic silicone check valves must undergo complete physical inspection every 5,000 operating hours or 24 months, whichever comes first. If check valves exhibit stiffness, discoloration, or loss of backflow sealing efficiency under a 5 PSI reverse pressure test, replace them immediately to prevent product tank contamination.
Step-by-Step Guide to Understanding the Inogen One G5 Parts Diagram
Identify – Locate the specific component code on the Inogen One G5 parts diagram layout.
Locate – Position the oxygen concentrator on an antistatic work surface and remove the external battery pack.
Reference – Cross-reference the diagram structure to trace internal silicone tubing paths and wiring configurations.
Connect/Route – Route replacement sensor wiring and pressure lines precisely through designated internal housing channels.
Verify – Perform a pressure leak check and verify flow rate output settings using an oxygen analyzer.
Troubleshoot – Check fault codes on the LCD screen if oxygen purity drops below 87% post-assembly.